26-Station Refrigerator Door PU Foaming Line — refrigerator cabinet & door pu foaming lines by UREXCEED. Lead time 120 – 180 days, MOQ 1 line.
26-Station Refrigerator Door PU Foaming Line
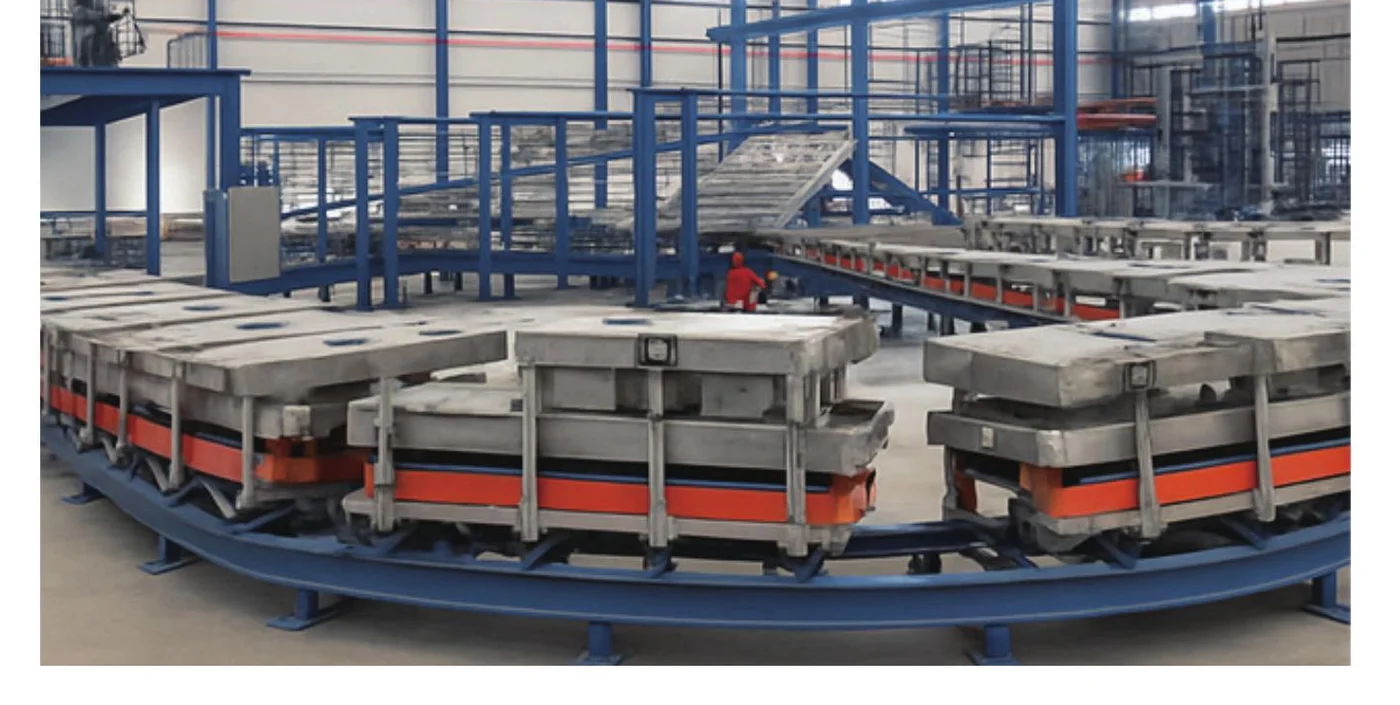
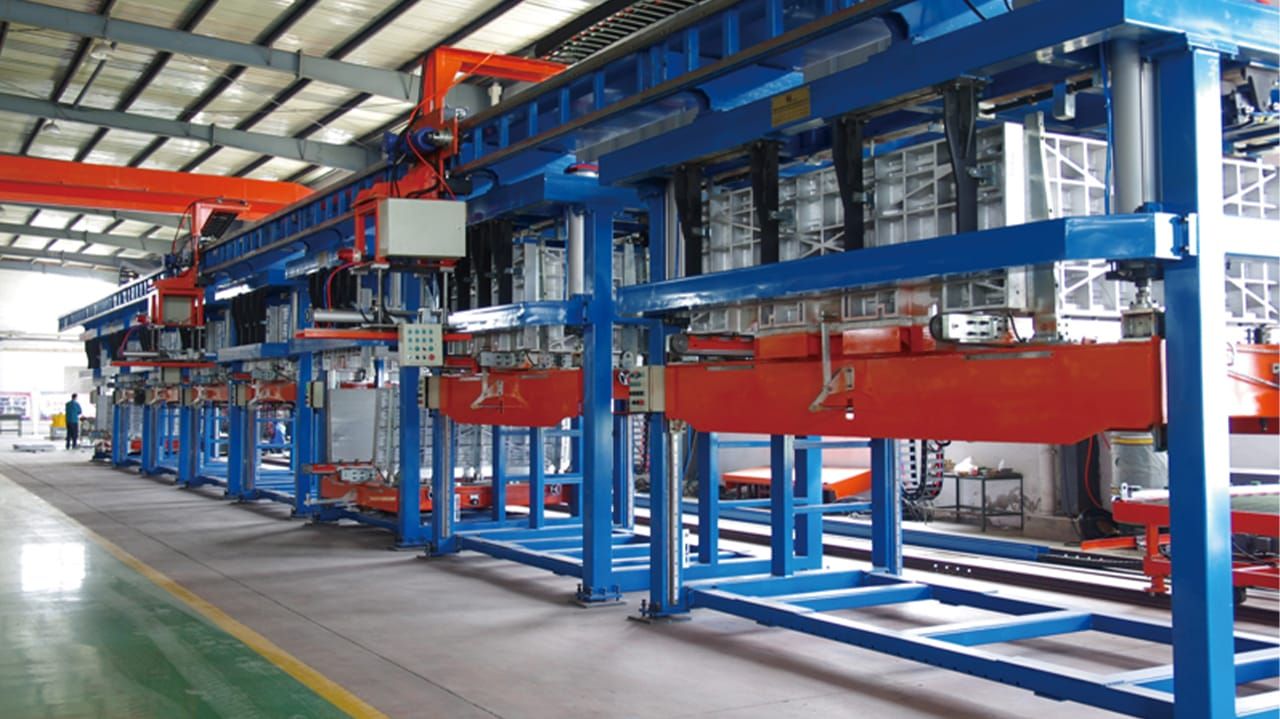
Closed-loop ground-rail PU foaming line dedicated to refrigerator and cabinet DOOR foaming. 26 single-cavity fixture stations on a continuous steel track, 20-sec takt, ~1,200 doors per 8-hour shift (~2,450/day on two shifts) at 85% line efficiency. 2,000 × 900 mm fixture × 200 mm closing height — sized for door panels. Cyclopentane + ATEX Zone 1, steam or oil heating.
See how this line fits the Refrigerator PU Foaming Solution →Start with an engineering scope review
Send dimensions, target output and drawings. Response timing follows project complexity and working hours.
Spesifikasi Teknis
- Layout Form
- Ground rail (closed-loop track around the foaming room)
- Overall Dimensions (L×W×H)
- Approx. 29,500 × 7,950 × 3,350 mm
- Number of Stations
- 26
- Production Cycle Time
- 20 seconds per door — single-cavity fixture, one door per takt (excluding manual operation time)
- Fixture Template Size
- 2,000 × 900 mm (per station)
- Mold Closing Height
- 200 mm (customizable on request)
- Heating Method
- Steam heating or oil mold temperature controller heating
- Foaming Material
- POL + Cyclopentane + ISO, or POL + 141b + ISO
- Injection Method
- Manual vertical pouring with mold open
- Steam Capacity
- 200 m³/h
- Curing Oven Temperature
- 55 ± 5°C
- Steam Temperature
- 120 – 150°C
- Compressed Air Requirement
- Working pressure ≥ 0.5 MPa, air flow approx. 0.1 m³/min
- Power Consumption
- Steam heating ~25 kW (380V 50Hz) · Oil heating ~145 kW
- Best Fit Capacity
- ~1,200 doors per 8-hour shift at 85% line efficiency (single-cavity, 20s takt — station count sets dwell/curing time, not rate); ~2,450/day on two shifts. See throughput calculator for your own takt and efficiency.
- Lead Time
- 120 – 180 days
- MOQ
- 1 line
Aplikasi
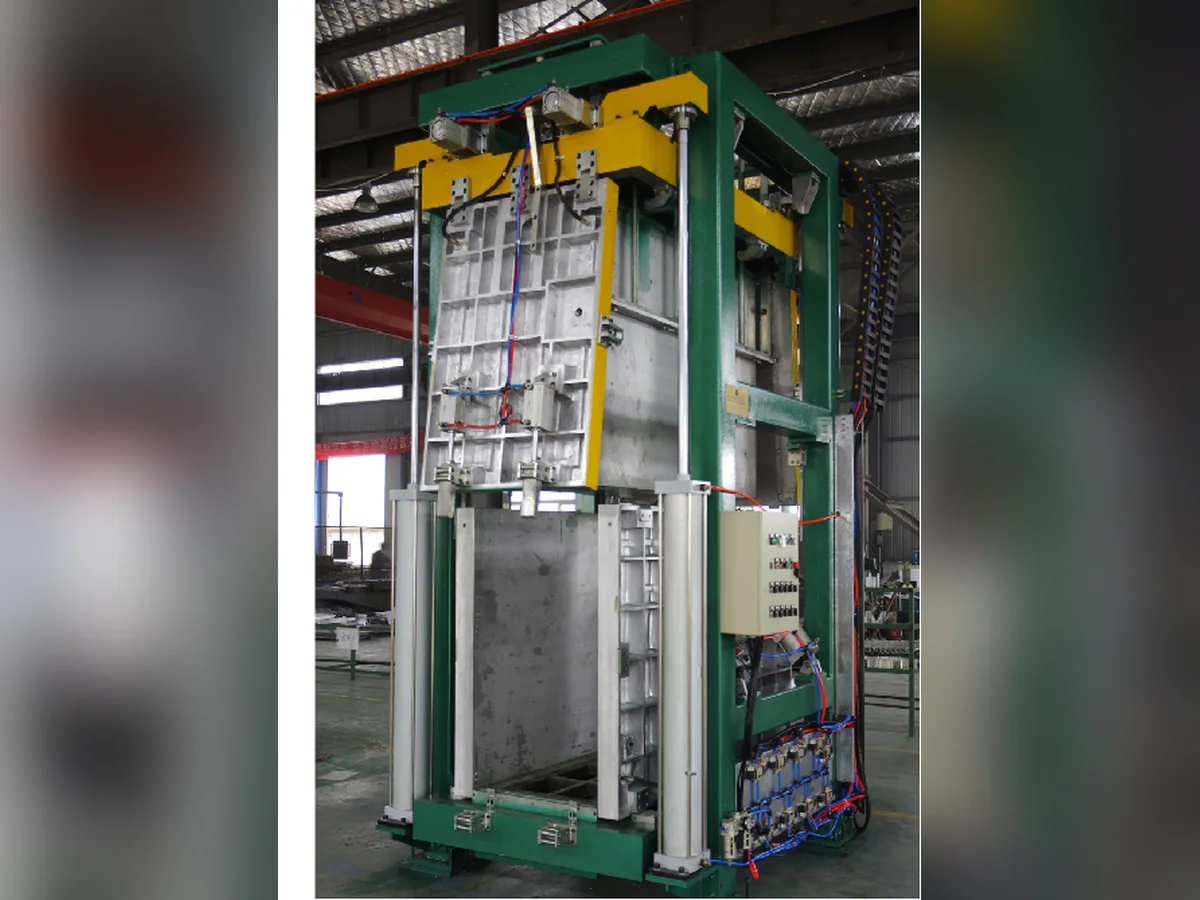
- Closed-loop ground-rail track design — 26 door fixture carriers move on a continuous steel rail around the foaming room; carriers cycle without backtracking, giving uniform throughput
- Fixture envelope sized for refrigerator door panels — 2,000 × 900 mm fixture template + 200 mm mould closing height accommodate door wall thicknesses 25–80 mm (single-door, French-door half, freezer lid all supported)
- Closed-loop steel rail and carrier underframes configured for the approved door fixture load and maintenance access
- 26 modular fixture stations — approved solid-door and insulated-lid mould variants mount on the agreed fixture pattern; per-station heated platen with temperature control
- Steam OR oil heating subsystem — your choice depending on factory infrastructure (steam = 25 kW if you have an existing boiler; oil = 145 kW standalone, no steam plant needed)
- High-pressure PU injection station — Cyclopentane-blown POL + ISO with ATEX Zone 1 envelope, LEL gas detection, N₂ blanket on storage tanks; vertical pouring with mould open + closing on injection
- 20-second station-to-station cycle, single-cavity fixture — engineered for refrigerator OEM factories producing high-volume DOOR output (~1,200 doors per 8-hour shift, ~2,450/day on two shifts, paired with separate cabinet body foaming)
- ~230 m² production envelope (29.5 × 7.95 m × 3.35 m H) + PLC / Profinet integration with upstream door-panel press, downstream gasket-fitment / heated-frame / final assembly stations
Integrated foaming equipment
Cyclopentane High-Pressure PU Foaming Machine
Our flagship — purpose-built for refrigerator factories chasing the top EU energy classes (B–C on the 2021 A–G label, formerly A+++). Cyclopentane-ready out of the box with full ATEX Zone 1 safety package. Three sizes covering 500 to 8,000 cabinets a day.
Why cyclopentane (and why it's the default choice for refrigerator factories now)
Cyclopentane is the blowing agent that won the refrigerator industry. About 70% of new refrigerator factories worldwide spec it. Here's the short version of why we built this machine cyclopentane-first.
Cost
Cost: roughly 1× the baseline. HFO-1233zd(E) runs 2.5–3×, HFC-245fa 2× — and HFC is being phased out anyway. On a 500,000-unit-per-year factory, cyclopentane saves USD 1.5–3M a year in raw material cost vs HFO.
Performance
Performance: lowest achievable k-factor of any commercial blowing agent (0.018 W/m·K), which means you can hit the top EU classes on the 2021 A–G label (B–C, formerly A+++) / Japan Top Runner / Australia 4-star without exotic formulation tricks.
Regulation
Regulation: allowed everywhere except a few EU markets that mandate HFO from 2025. The list of "cyclopentane forbidden" countries is essentially zero — the list of "HFC phased out" countries grows every year.
The trade-off
The trade-off: cyclopentane is flammable. Your foaming room becomes a hazardous zone. That's solvable engineering (ATEX equipment, gas detection, ventilation) but the room and the machine both need it. Our machine ships with that whole package built in.
What's inside our cyclopentane high-pressure machine
The whole machine is engineered around safely running cyclopentane day-in day-out for 10+ years. Eight major sub-systems, all built to handle the flammability while delivering ±0.5% metering accuracy.
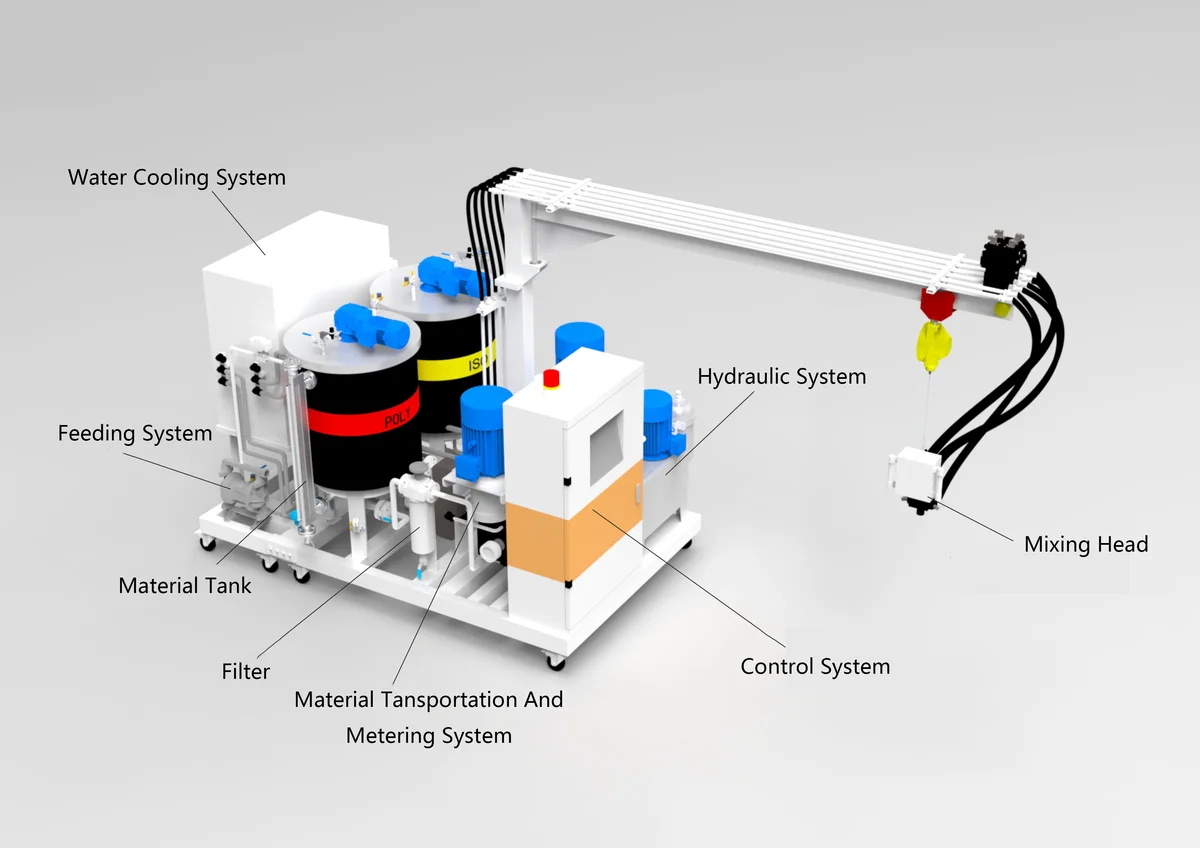
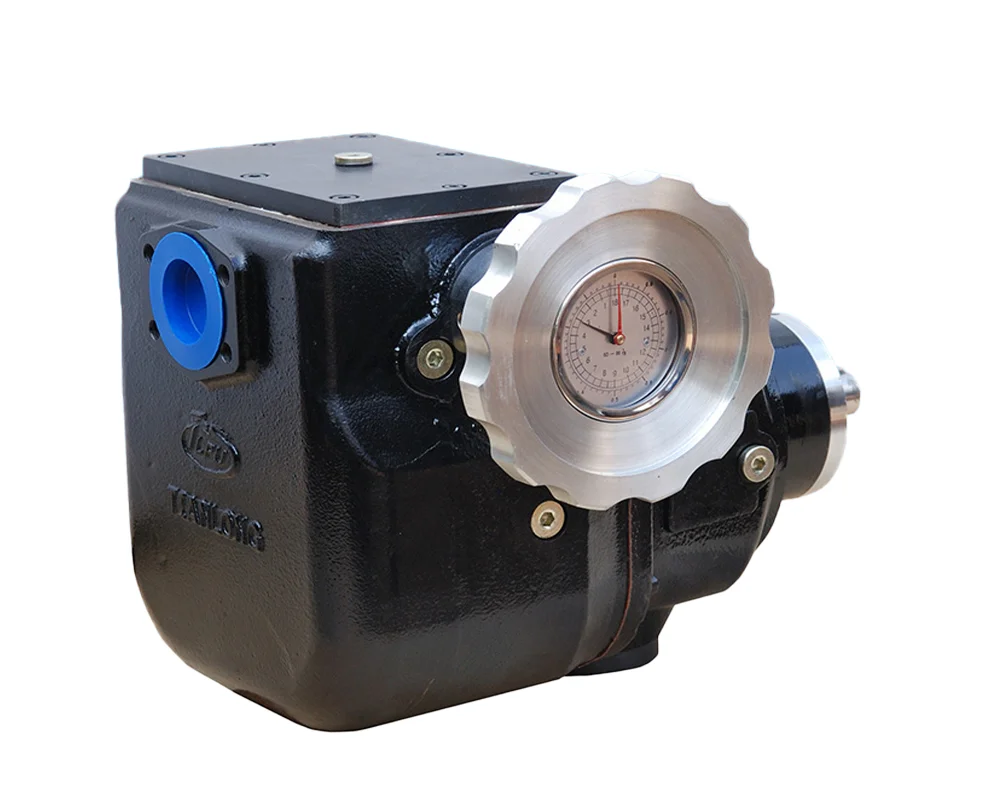
Metering pumps
High-pressure axial piston pumps (Bosch Rexroth A10VSO series) — servo-driven, ±0.5% metering accuracy. We use the same pumps as the major European brands because nothing else in this class delivers the consistency a refrigerator line needs.
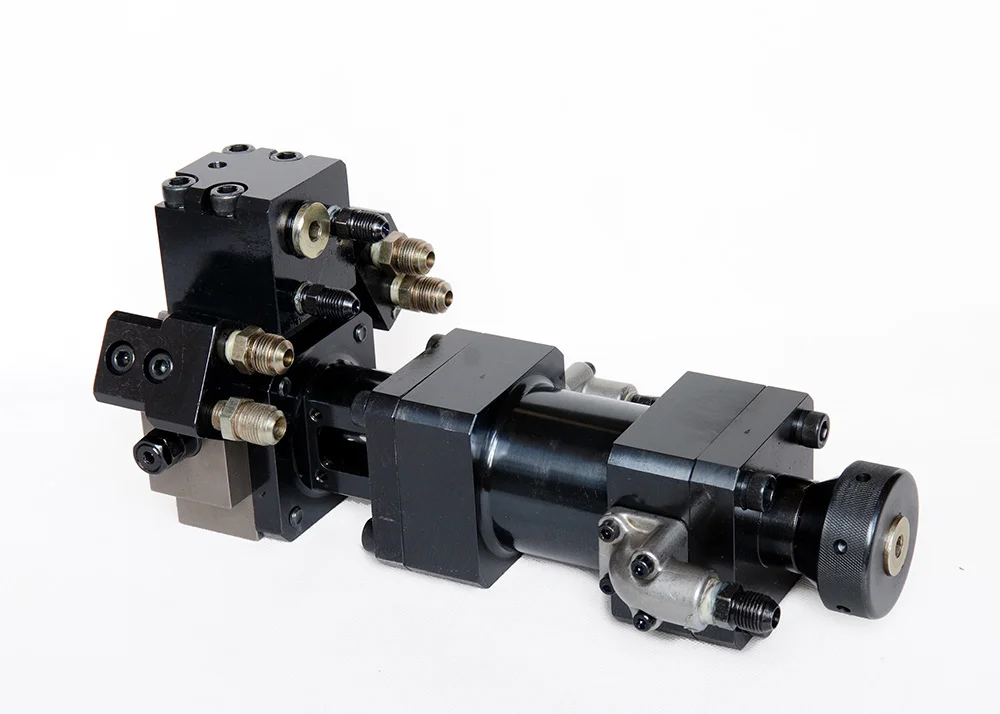
Mixing head (L-type and T-type available)
Self-cleaning mixing head — hydraulically actuated cleaning rod after every shot, no solvent needed. Standard 2K head; 3K and 4K available if you need to inject color or trace additives.
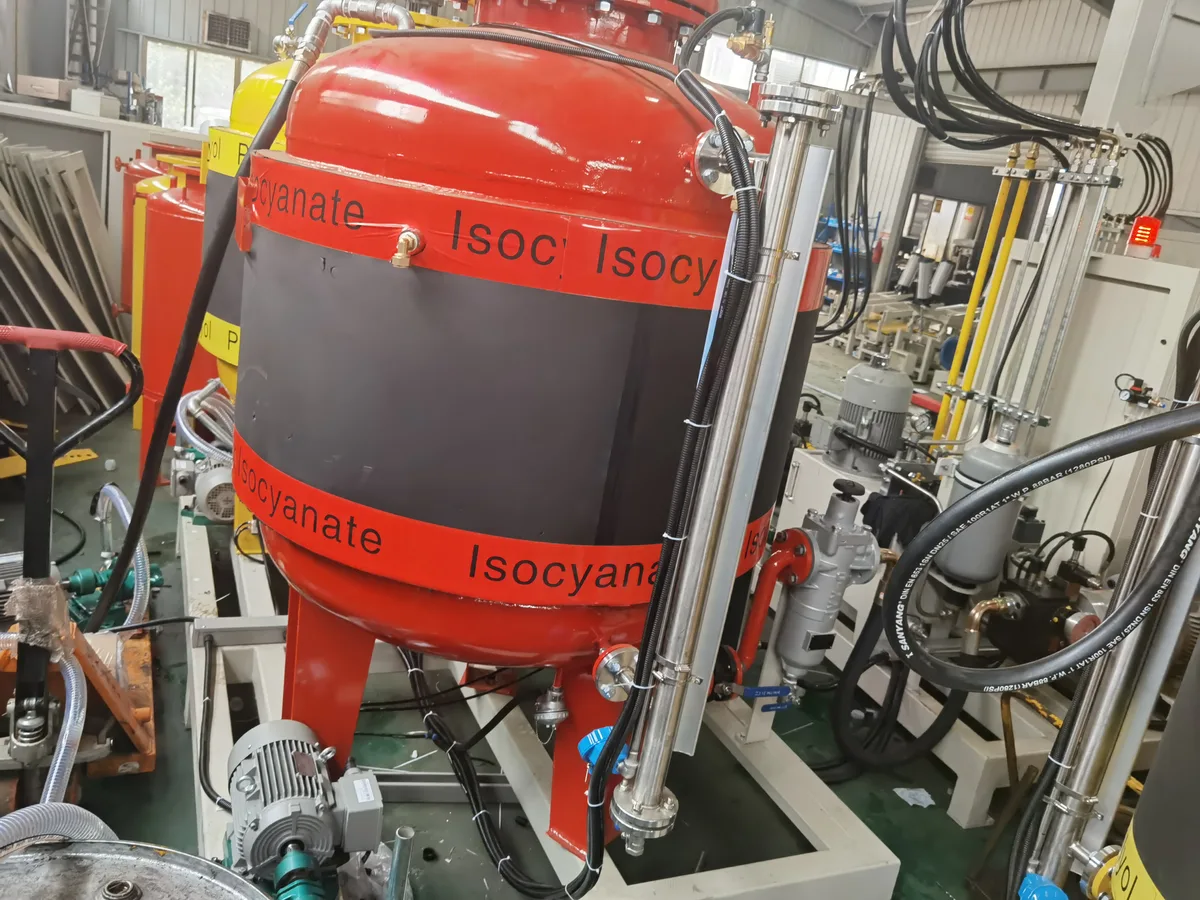
Day tanks (Polyol + ISO)
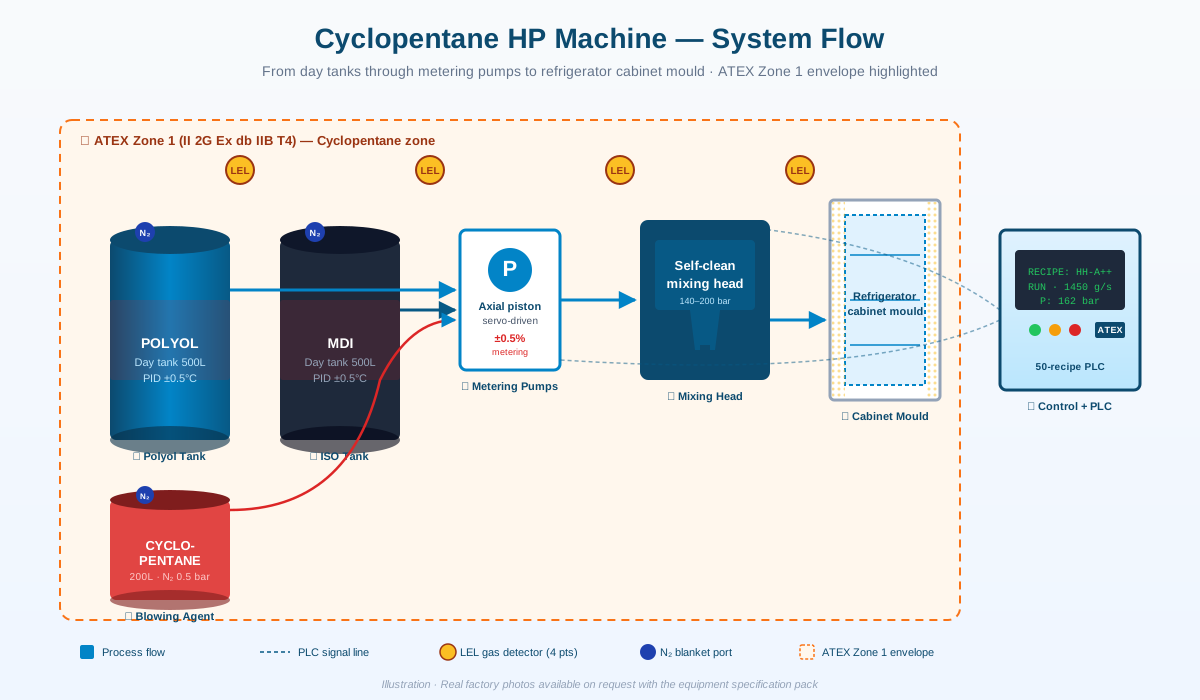
Jacketed day tanks (250 / 500 / 1,000 L per component) — chilled water + electric heater dual loop, PID ±0.5°C. The cyclopentane tank gets a closed N₂ blanket at 0.3–0.5 bar to prevent oxygen ingress and pressure variance.
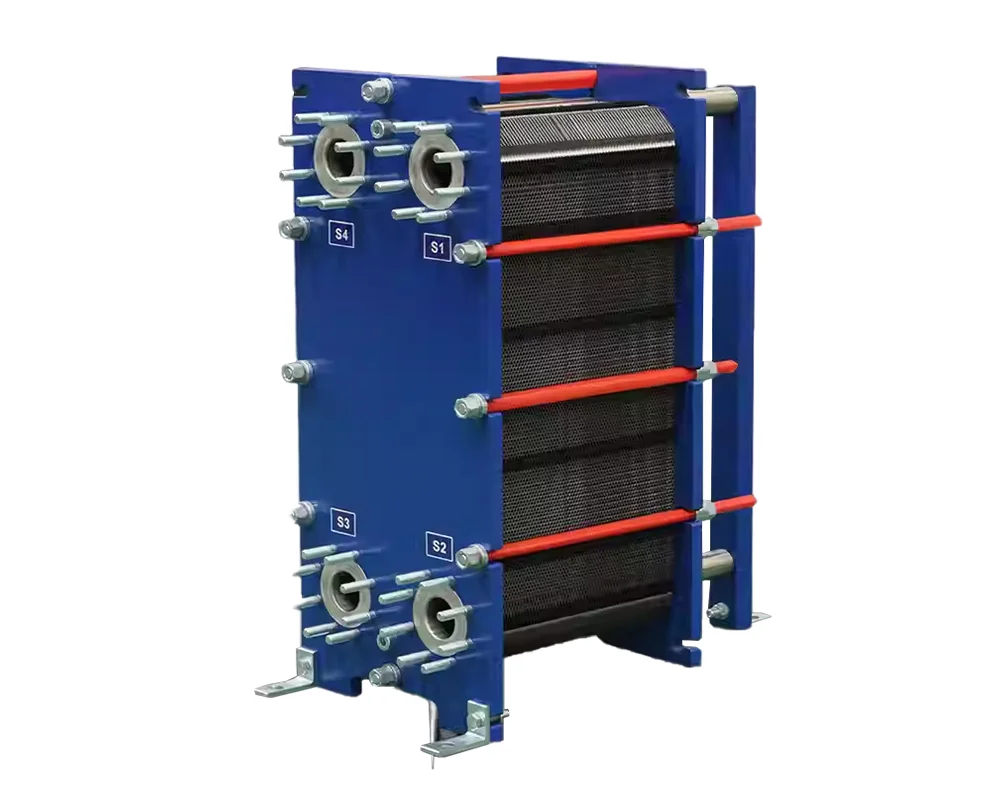
Cooling / heat exchangers
Cooling circuit with chiller — handles the heat of compression on the pumps. A typical 1,500 g/s machine draws 6–8 kW of cooling capacity. We size it for your local ambient (40°C design point in Middle East / Africa, 30°C in Europe).
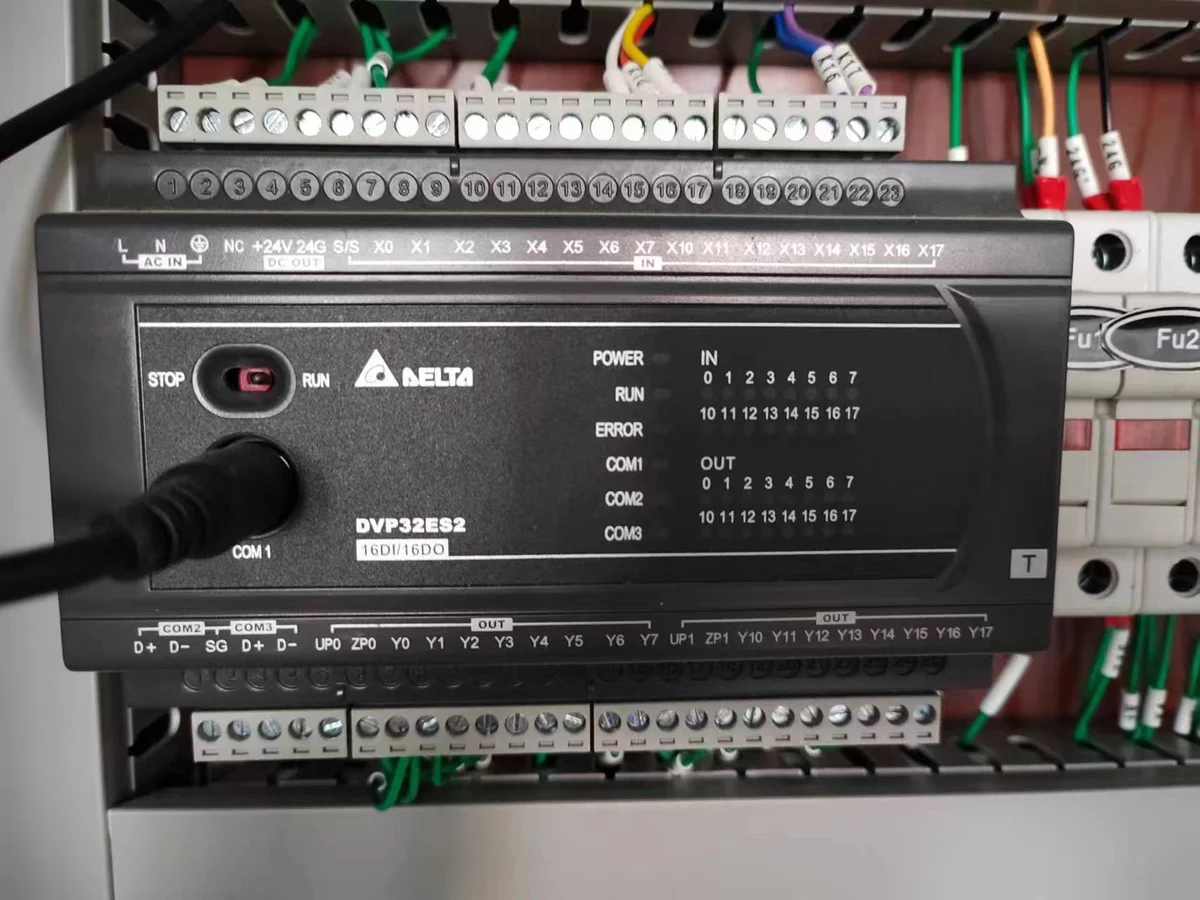
PLC + HMI · ATEX electrics
PLC + HMI (Siemens S7-1500 or Mitsubishi Q-series, your choice) with 50-recipe storage. Switch between cabinet recipes in under 30 seconds. Production logging with 1-second granularity, exportable to your MES. ATEX-rated electrical enclosure (II 2G Ex db IIB T4, Zone 1 inside) — every cable, junction box, sensor and motor in the cyclopentane zone is rated for explosive atmosphere. Gas detection sensors at 4 points trigger auto-alarm at 25% LEL and auto-shutdown with N₂ flooding at 50%.
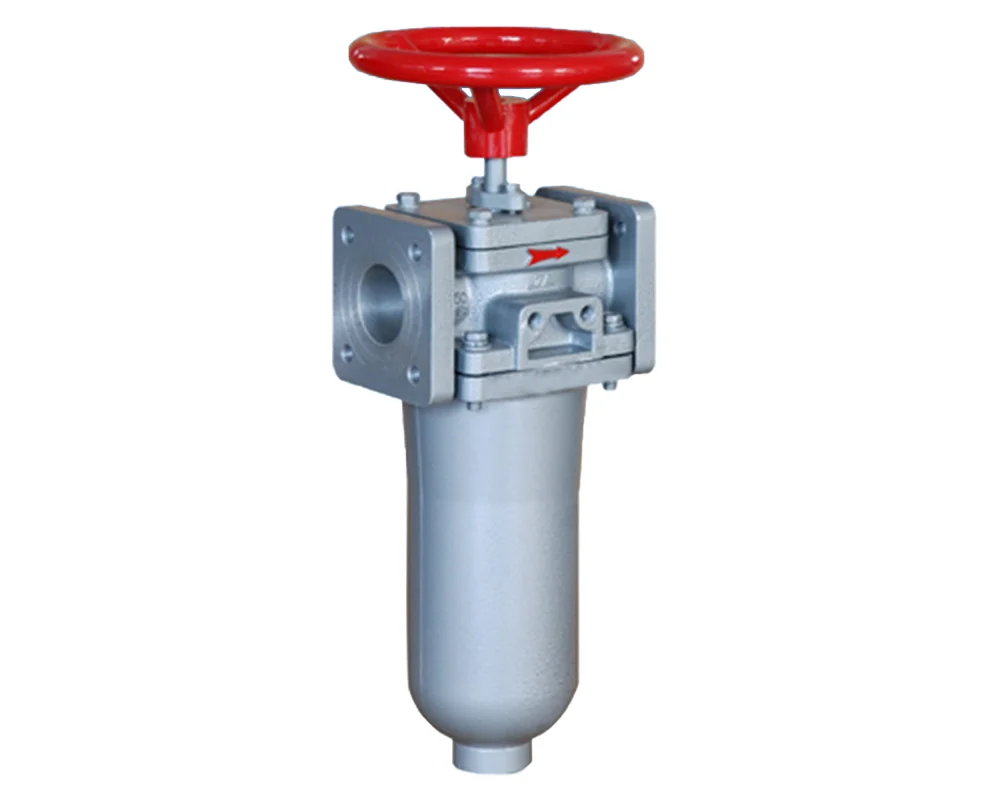
Feed-line filters · CIP cleaning
CIP (Clean-In-Place) self-cleaning cycle — programmable solvent flush of the mixing head, hoses, and pump heads for end-of-shift or recipe-change cleaning. Reduces manual intervention by 80%. Nitrogen distribution & blanket system — single N₂ supply feeds the polyol tank, cyclopentane tank, mixing head purge, and emergency shutdown flood. We provide the nitrogen generator if your plant doesn't already have N₂ infrastructure.
▸ See the full system flow diagram (illustration)
The ATEX safety package — what your fire department will want to see
Cyclopentane is flammable. Your foaming room becomes a Zone 1 (continuous risk) inside the equipment envelope and Zone 2 (occasional risk) outside it. Most refrigerator buyers spend more time worrying about ATEX approval than about the machine itself. Here's how we make that easy.
Enclosure & electrics
Every electrical component in the Zone 1 envelope is rated II 2G Ex db IIB T4. Standard junction boxes, motor terminations, sensor housings — all certified. We supply the EU type-examination certificates as a PDF pack.
Gas detection
LEL gas detectors at four points around the machine (under the mixing head, near the cyclopentane tank vent, near the day tank manhole, near the pump bay). Calibrated at install, calibration record stays with the machine documentation.
Alarms & shutdown
Auto-alarm at 25% LEL (visual + audible, machine slows down). Auto-shutdown at 50% LEL (machine stops, mixing head locks open, N₂ flood activates, your fire panel gets notified via dry contact).
Ventilation spec
We don't supply the room ventilation but we provide the design spec: minimum 6 air changes per hour, exhaust at floor level (cyclopentane vapor is denser than air), all electrical in the room ATEX-rated to match the zone classification.
Operator training
Every machine ships with operator training material covering ATEX-specific procedures — what to do if an LEL alarm fires, how to isolate the cyclopentane tank, emergency manual N₂ flood. We train your operators on this during commissioning.
Past approvals
We've passed ATEX approval (or equivalent local fire approval) at refrigerator factories in EU, Russia, Turkey, Brazil, Saudi Arabia, Egypt, Vietnam, Indonesia, India. Past approval files are available — they make your local approval process much faster.
Three machine sizes mapped to your daily cabinet output
Pick by daily output, not by gut feel. Oversizing wastes capex and gives slow cycle times; undersizing creates bottlenecks. Here's how we sit it with our refrigerator factory customers.
| Machine size | Output (g/s) | Daily cabinets | Factory type | Power draw |
|---|---|---|---|---|
| UPM-HP-500 | 100 – 500 | 500 – 2,000 cabinets/day | Small / mid-size factory, single shift | ~15 kW |
| UPM-HP-1500 | 200 – 1,500 | 2,000 – 5,000 cabinets/day | Mainstream household refrigerator OEM, 2-shift | ~25 kW |
| UPM-HP-3000 | 500 – 3,000 | 5,000 – 8,000+ cabinets/day | Large multi-line plant, 3-shift continuous | ~40 kW |
If your output mix includes very different cabinet sizes (e.g. 200L bottom-mount + 700L French-door on the same line), we may recommend two smaller machines rather than one big one — quicker recipe changeover, less waste during shot-weight transitions.
How we deliver a top EU energy class (B–C on the 2021 label, formerly A+++) on this machine: the parameter table
Energy class is a recipe problem, not a machine problem. Same machine can land at the top of the EU A–G label or three classes lower depending on how you set it up. Here's the parameter table we hand out with every machine + matching PU system shipment.
| Target class | k-factor | Molded density | Cream time | Gel time | Mould temp |
|---|---|---|---|---|---|
| EU B–C (2021 label, former A+++) / JP Top Runner | 0.018 W/m·K | 32–35 kg/m³ | 7s | 42s | 42–45°C |
| EU D–E (mainstream, former A++) | 0.020 W/m·K | 35–38 kg/m³ | 8s | 45s | 40–45°C |
| EU E–F (former A+) / value lines | 0.022 W/m·K | 38–40 kg/m³ | 9s | 50s | 38–42°C |
Pump pressure (~160 bar typical), shot weight (varies by cabinet, 600–1,200g), and ISO-to-polyol ratio (1.05–1.15:1) are tuned in commissioning. The PLC stores all of this as a named recipe — your operator picks the cabinet from a list, the machine sets itself.
Installation, commissioning, training: what happens after the container lands
Civil works, machine assembly, first-batch foaming, operator training — about 6–10 weeks from container arrival to handing the line over to your team.
- 1
Week 1–2 — Civil works at your site (foundation pad, N₂ supply, electrical hookup, ventilation, drainage). We send a printed checklist + drawings before container ships.
- 2
Week 3 — Container arrives. Two of our engineers fly in. Crane the components off the container, position on the foundation, connect piping and electrical.
- 3
Week 4 — Cold commissioning: power up, leak tests, calibration of gas detectors, calibration of pumps. ATEX inspection by your local authority happens here if required.
- 4
Week 5 — Hot commissioning: first foaming runs with water-blown trial recipe (no cyclopentane yet, just to validate the mechanics). Then switch to cyclopentane, run 50 trial cabinets.
- 5
Week 6 — Operator training (4–6 people, mix of foaming operators + maintenance + line supervisor). About 3 days of classroom + 2 days hands-on.
- 6
Week 7 — Production ramp. Our engineers stay through the first 100 production cabinets. Sign-off and handover after.
- 7
Week 8 onward — Remote support via PLC remote diagnostics. Engineer return visit at 3 months and 12 months included free.
Spare parts, service, the long-game cost picture
The machine is built to run for 10+ years on a 3-shift refrigerator factory. Here's the ongoing cost shape so you can budget properly.
Warranty
Standard warranty: 2 years on pumps, mixing heads, PLC. 1 year on wear items (seals, filters, gas detectors). Extended 4-year warranty available at order time (+5% of equipment cost).
Spare parts kit
Recommended spare parts kit at order: about 5% of machine cost. Covers 2 years of routine wear (seals, O-rings, filter elements, mixing head wear plates, LEL sensor head replacement).
Stock locations
We stock buffer spares in three locations: Shanghai (main warehouse), Istanbul (covers EU / Russia / MENA), Dammam (GCC + East Africa). Critical parts ship in 2–5 days.
Remote diagnostics
Remote diagnostics included for 2 years (free), then USD 3,000 / year. Lets us pull PLC logs and walk your operator through fixes without a site visit. About 70% of issues we resolve this way.
Routine maintenance
Routine maintenance cost: 2–4% of equipment cost per year for wear parts. Heavier service (pump rebuild, mixing head overhaul) every 4–5 years runs another 5–8%.
Operator training refreshers
Refresher training for new operators: USD 500 / day at your site, free remote sessions. We also keep training videos on a private channel for your team.
Why this machine works best with our PU system
A machine and a chemistry that have never worked together still need 1–2 months of mutual calibration. We ship our machine pre-tuned for our PU system — saves you that integration time, gives you one supplier accountable for the whole foam result.
Formulation match. Our cyclopentane-grade polyol is formulated against the metering characteristics of this exact machine — pump compatibility, shear sensitivity, gel time matched to standard cabinet cycle times.
Parameter card with every shipment. Every PU shipment includes a parameter card listing target machine settings for that batch (tank temperatures, mixing pressure, shot weight, cream/gel/tack-free time). Your operator dials those settings on this machine's HMI — no R&D needed.
One supplier, one accountability. When something goes wrong with foam quality, you have one supplier to call. We can't blame the chemicals if you have a machine issue, and vice versa.
Four Pain Points Refrigerator Factory Founders Bring Us About PU Foaming Lines
These are the recurring frustrations we hear when refrigerator factories switch from manual or batch foaming to a continuous PU line.
Bottleneck at the foaming station — line speed limited by curing time
Manual / single-station setups force the entire factory to wait while each cabinet cures (5–10 min). Our multi-station lines (6–26 stations) decouple injection from cure: while station 1 is injecting, stations 2–26 are curing in parallel. Throughput jumps 5–10× without buying more PU machines.
Foam quality drifts shift-to-shift — operators tune by hand and recipe walks
Without temperature-controlled fixtures and metered PU dispensing, every operator settings drift compounds. Our line ships with PID ±0.5°C fixture temperature + ±0.5% PU metering accuracy + locked recipe storage in the PLC. Shift-to-shift variance drops from ±8 kg/m³ foam density to ±1 kg/m³.
Cabinet wall thickness variance fails type-test (EU 2019/2024 Ecodesign)
Type-test failures cluster around wall thickness variance > ±2 mm. Our line's combination of cast aluminium moulds (±0.05 mm cavity), temperature-controlled fixtures (±0.3 mm parallelism), and metered PU drops final wall thickness variance to ±0.3 mm. Type-test pass rate on first submission: 90%+.
Switching from HFC to cyclopentane breaks our existing line
EU F-gas regulations from 2025 force most factories off HFC-245fa. Adapting an old non-ATEX line costs USD 600K–1M in retrofits. Our cyclopentane-ready lines ship with ATEX Zone 1 electrics, LEL detection at 4 points, and N₂ blanket on day tanks — included in base line price, not an add-on.
How the line operates — stations, cycle, integration
A PU foaming line is more than just "moulds and a foaming machine bolted to a conveyor". It's a coordinated dance of cabinet loading, mould closing, PU injection, curing oven, demould, and cabinet release — all on a timed cycle. Here's the actual workflow.
- 1
Cabinet loading station
Pre-formed steel cabinet shell + ABS/HIPS inner liner enters the line. Operator (or robot) positions the cabinet on the mould fixture, aligns it via locating pins, locks the front and rear baffles. Takes 8–12 seconds per cabinet.
- 2
Mould closing + clamping
Mould top half lowers onto the cabinet, side-locking wheels engage, pneumatic mold locking activates. Clamping force builds to 1–5 tons depending on cabinet geometry. Heated platen reaches working temperature 40–60°C.
- 3
PU injection
Mould moves to injection station. PU foaming machine high-pressure mixing head injects POL + Cyclopentane + ISO mix through the gate. Single shot of 300–800 g depending on cabinet volume. Cream time 6–8 sec; gel time 35–50 sec; the cabinet then moves to the curing oven before tack-free.
- 4
Curing oven travel
Cabinet rides the conveyor through a 55 ± 5°C heated oven (steam or hot air). Foam fully cures in 5–8 minutes depending on cabinet wall thickness. Multiple stations in parallel — while one cabinet is curing, the next is being injected.
- 5
Demould + release
Mould opens, demould assist mechanism lifts the cabinet free, conveyor transports to downstream evaporator/condenser assembly line. Mould returns to loading station, ready for next cabinet. Total round-trip station-to-station: matches the line's cycle time spec.
How the line pairs with our moulds, fixtures, machines, and PU chemicals
A PU foaming line is the integration platform — it doesn't work alone. Here's how the catalog §03 moulds, §04 mold fixture, §05 PU machines, and §02 raw materials snap together on this line.
The 6 refrigerator cabinet moulds (catalog §03) bolt directly to fixture plates on each station. Standard mounting pattern fits all our moulds; adapter plates available for non-UREXCEED moulds.
View product →The mold fixture (catalog §04) is one fixture per station — ground rail has 26, linear has 6–8, rotary door has 7–8. Each fixture is independently temperature-controlled.
View product →The cyclopentane high-pressure PU foaming machine (catalog §05) sits at the injection station and feeds via heated transfer hoses to each mould. One machine serves one line; for redundancy, factories may install a backup.
View product →PU raw materials (POL + Cyclopentane + ISO) are stored in 22.5-ton ISO tanks (polyol, MDI) + cyclopentane day tank, all with N₂ blanket and PID temperature control. Material consumption for a 26-station ground rail line at full capacity: ~30 tons polyol + ~30 tons MDI + ~3 tons cyclopentane per month.
View product →When you order moulds + fixtures + PU machine + materials + line together, we calibrate the whole stack at our factory before shipment. Cuts on-site commissioning time from 8 weeks to 2–3 weeks.
Steam heating vs oil heating — running cost reality
Ground rail lines can be configured for steam heating (25 kW power draw) or oil heating (145 kW). The 6× power-consumption gap looks dramatic, but the real total-cost-of-ownership picture depends on your existing factory infrastructure.
| Aspect | Steam Heating | Oil Heating |
|---|---|---|
| Equipment cost | ~baseline | ~baseline (similar) |
| Line power consumption | ~25 kW | ~145 kW |
| Boiler / heater capex | High (need separate steam boiler if no existing) | Built-in electric heater, no extra capex |
| Running cost (cheap electricity, no steam) | High capex but low ongoing | Low capex, moderate ongoing |
| Running cost (existing steam plant) | Very low (marginal cost) | Wasteful (paying for electric heat you don't need) |
| Best fit | Existing steam-infrastructure factories | Factories without steam, cheap electricity |
Rule of thumb: if your factory already has a steam boiler running for other processes (curing rooms, washing, sterilization), add steam heating to the foaming line — marginal cost is near zero. If you're a greenfield factory in a region with cheap industrial electricity (USA, parts of Europe, Middle East), oil heating saves the boiler capex.
Installation timeline — from PO to first cabinet rolling off the line
A refrigerator PU production line is a 10–14 week project from purchase order to first foamed cabinet. Here's the realistic timeline with each milestone.
Week 1–2: Design freeze — finalize line layout, mould fixture spec, civil works drawing. We send foundation drawing + utility hookup spec to your contractor.
Week 3–6 (parallel): Civil works at your site (foundation pad, drainage, utilities). Equipment fabrication at our factory.
Week 5–10: Sea freight shipping (4–6 weeks transit depending on port).
Week 10–12: On-site installation by our 3–5 engineer team — 1–2 weeks for linear / rotary door, 2–3 weeks for ground rail.
Week 12–14: Commissioning + first 20–50 trial cabinets + operator training. Sign-off and handover.
Ongoing: Remote diagnostics free for 24 months. Engineer return visit at 3 months and 12 months included.
Optional upgrade modules — extend a base line without buying a new one
The base line covers the foaming workflow end-to-end. These modular add-ons slot in at specific stations to unlock additional capacity or quality control.
Automatic mould release dispenser — robotic spray of release agent before each cycle. Cuts manual operator step, improves coating uniformity. +USD 18K–35K. Pays back in 8–14 months at 1,500+ units/day.
ABB / KUKA 6-axis robot integration — robotic mould loading, demoulding, palletizing, or insertion of internal components (evaporator, condenser). +USD 80K–180K per robot. Boost throughput +30%, cut labor 4 operators per shift.
Full sensor + traceability pack — embedded thermocouples + pressure sensors per station + PLC data logging + cabinet serial-number-to-batch traceability. +USD 40K–80K. Required for medical refrigerator / ULT / regulated markets.
Auto-demould assist mechanism — pneumatic lifters that pull cabinets free from mould without operator handling. +USD 22K–48K. Reduces cabinet damage rate from 1% to <0.1%.
Vision-based quality inspection — 4-camera scan of each cabinet (wall thickness, surface defects, dimensional accuracy) before line exit. +USD 60K–120K. Catches 95%+ of foam defects before downstream assembly.
In-line foam scrap recycling — grinds foam offcuts back into raw material feed (up to 8% recycled content). +USD 35K–60K. Cuts raw material cost 5–7% and meets EU PEF recycled-content thresholds.
Customization — line layout adapted to your factory and capacity target
No two refrigerator factories are identical. We customize the line on 5 axes so you don't over-spec capacity you don't need or under-spec capacity you can't expand later.
Station count
Station count — 6 (linear / rotary) / 12 (small ground rail) / 18 / 26 (full ground rail). Pick by daily output target (500–10,000 cabinets/day). Modular backbone — add stations later as production scales.
Factory layout
Factory footprint — straight L-rail (60–80 m long, narrow factory) / parallel double-rail (compact 30 m × 20 m, wide factory) / rotary hub (15 m radius circular, square factory). Our engineers design to your floor plan.
Cabinet SKU mix
Cabinet SKU mix — single-SKU (highest throughput, fixed mould fixtures) / multi-SKU (3–8 SKUs rotating through quick-change fixtures, 25–30% throughput hit). Pick based on your product line.
Heating method
Heating method — steam (cheap if factory has boiler) / electric oil (no boiler needed, 6× power draw) / hybrid. Choose at quote stage based on your factory utilities.
Automation tier
Automation tier — manual labor (4–6 operators per shift) / semi-auto with robot loading (2–3 operators) / full-auto with vision QC + auto-demould (1 operator monitoring). Capex scales 1× → 1.5× → 2× across tiers.
Service, warranty, and what happens 5 years later
A refrigerator PU foaming line is a 10–15-year asset. Here's the long-game support picture.
Warranty
Standard 24-month warranty on mechanical structure (rails, frames, lifting drives). 12-month on electrical/PLC components. 6-month on wear parts (seals, sensors, heating elements). Extended 4-year mechanical warranty available at order time (+5% line cost).
Spare parts kit
Recommended spare parts kit at order: ~3% of line cost. Covers 2 years of routine wear (seals, O-rings, sensor heads, heating elements). 24/7 spare-parts emergency hotline.
Spares locations
Critical spares stocked in Shanghai (main), Istanbul (covers EU / Russia / MENA), Dammam (GCC + East Africa). Critical parts ship in 2–5 days.
Remote diagnostics
Remote diagnostics included for 24 months (free), then USD 3,000–6,000/year. Pulls PLC logs, walks your operator through fixes, can take control of HMI to adjust settings remotely. About 70% of issues we resolve without an on-site visit.
Routine maintenance
Routine maintenance cost: ~2–3% of equipment value per year for wear parts. Heavier service (chain replacement on ground rail, bushing renewal on rotary hub) every 5–7 years runs another 5–8%.
Operator training refreshers
Refresher training for new operators: USD 500/day on-site, free remote sessions. Private training video channel with installation guides, troubleshooting, and SOP videos.
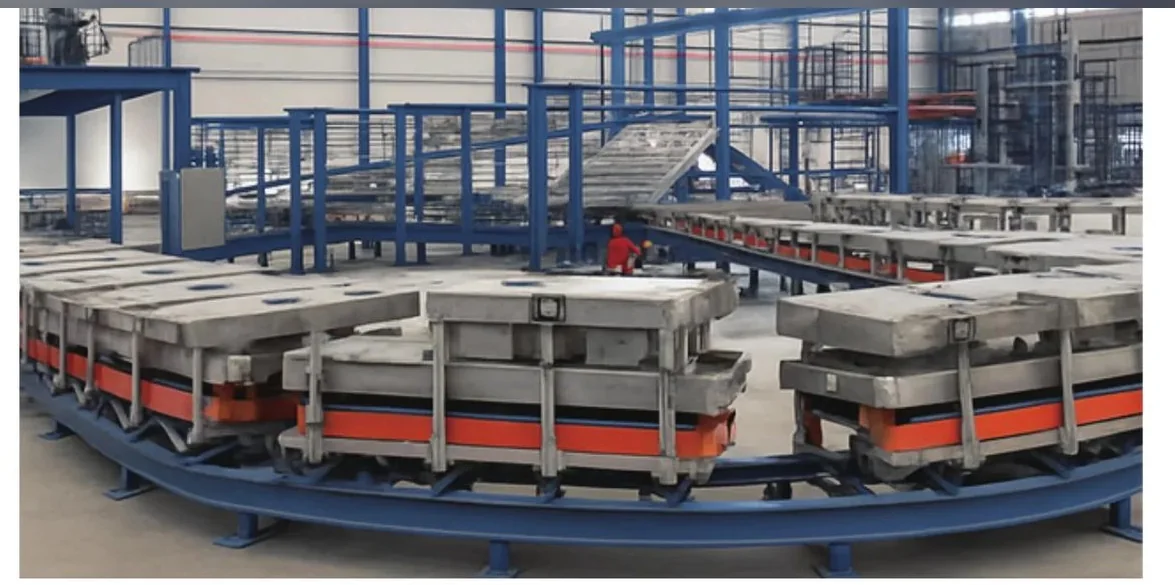
Inside the Line — Real Factory Photos (Not a Render)
These are unretouched photographs of an installed 26-station closed-loop ground-rail PU foaming line on a customer refrigerator-door foaming floor — the same continuous steel rail, carrier fixtures and heated platens described in the specification above. No CGI, no rotating render: what you see is what we build and ship.
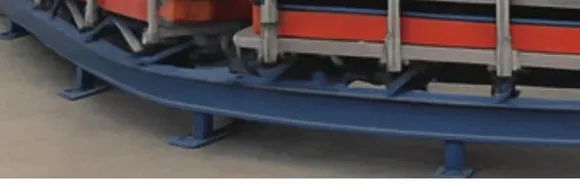
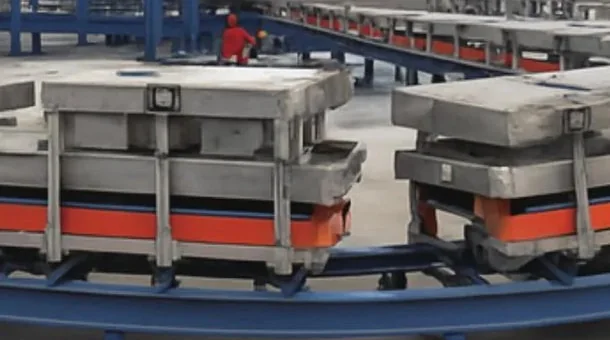
Four Refrigerator Door Applications This Line Foams — All Solid PU-Foam-Cored Panels
The 26-station ground-rail line foams SOLID PU-foam refrigerator door panels (steel skin / painted skin + PU foam core + plastic inner liner). Below: the four door applications our customers run on it most often. Glass-pane display doors, heated-frame merchandiser doors, and glass-top chest covers are NOT supported on this line — those need a different fixture and assembly.
Household Refrigerator Doors
Top-mount / bottom-mount / French-door solid panels for residential refrigerator OEM brands. The largest-volume door family — ~1,200 doors per 8-hour shift on a single-SKU run (single-cavity, 20s takt, 85% efficiency). Typical door wall thickness 50–70 mm, fixture envelope 1,700–1,900 × 600–800 mm.
Commercial Upright Refrigerator + Freezer Doors
Solid stainless / painted-steel doors for tall multi-door commercial refrigerators and freezers — back-of-house restaurant kitchens, hotel walk-ins, supermarket reach-ins. Single-door, double-door and triple-door variants share the same fixture pattern. Higher PU foam density (40–45 kg/m³ vs 36 kg/m³ on household) for −18°C freezer duty.
Chest Freezer Solid Lids
Top-opening solid-lid chest freezer panels (no glass) — household chest freezers, ice-cream commercial chests, vaccine cold-chain chests. Larger fixture footprint, deeper draft on the mould — line tolerates the wider geometry on the same 200 mm closing-height envelope.
Medical / Pharmaceutical Refrigerator Doors
WHO PQS-spec vaccine refrigerator doors, clinical-trial sample storage doors, pharmacy reach-in doors — all SOLID-DOOR variants (pharma-display glass-door units run on a separate line). Cyclopentane PU foam with 100% leak-test station downstream meets ASTM F1980 shelf-life simulation.
Produk Terkait
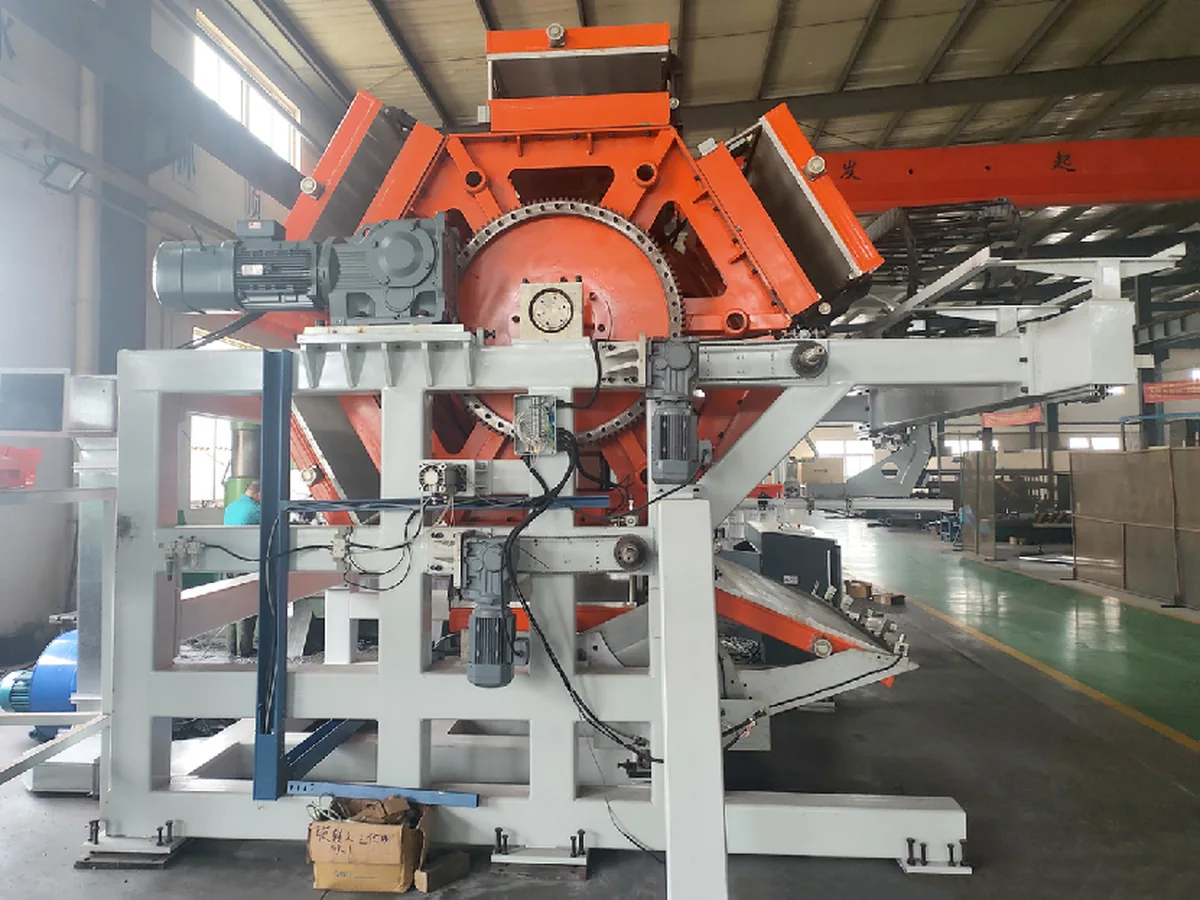
4-Station Hydraulic Air-Curtain Cabinet Foaming Fixture
4-station hydraulic foaming fixture for air-curtain refrigerated display cabinets (open-front merchandisers up to 4 × 1.8 × 0.55 m). Top/bottom flat-pressing clamp, water heating, 50 kW, 80–200 cabinets/shift.
Discontinuous Cold Room Panel Production Line — 1.2 m × 3/6/9/12/18 m PU Sandwich Panels
Discontinuous (intermittent press) PU sandwich panel machine — the complete press + PU foaming line — for steel / PU / steel cold-room panels. Panel width 1.2 m (industry standard). Five standard lengths: 3 / 6 / 9 / 12 / 18 m. Daily output 200–500 m²/shift per press. EN 14509 / ASTM E72 compliant. Best fit for factory owners building a new modular-cold-room or commercial cold-storage panel plant — not for high-volume continuous-belt operations.
Hydraulic Foaming Press — Specialty / Irregular Cabinets
Standalone hydraulic foaming press for air-curtain, wine cabinet and irregular / non-standard cabinet foaming. Water-heated + air-cooling, 50 kW, 40–120 cabinets/shift. Complements existing line for capacity peaking.
Cross-Sell · One-Partner Synergy
Match Your Production Line With Factory Solutions
Pick the factory type that matches your buyer market — we engineer the complete production line for that vertical.
Browse 13 Factory Solutions
Refrigerator / Chef Base / Freezer / Display Cabinet / Commercial Freezer + 8 specialized markets.
Learn more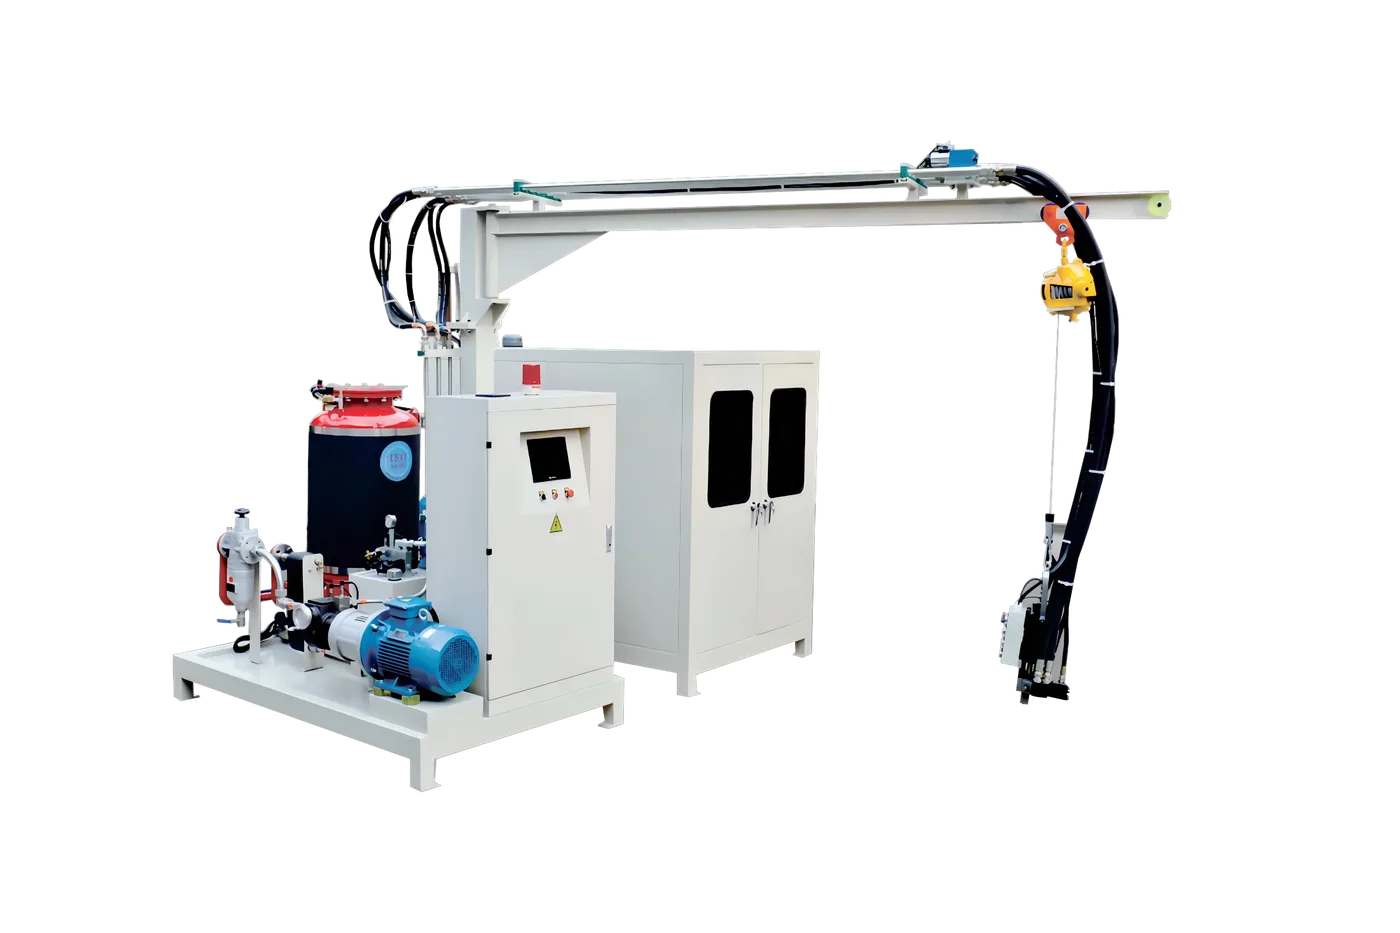
PU Foaming Machines
High-pressure (cyclopentane / 2C / 3C) + low-pressure + spray-foam — pick the foaming line that matches your factory.
Learn more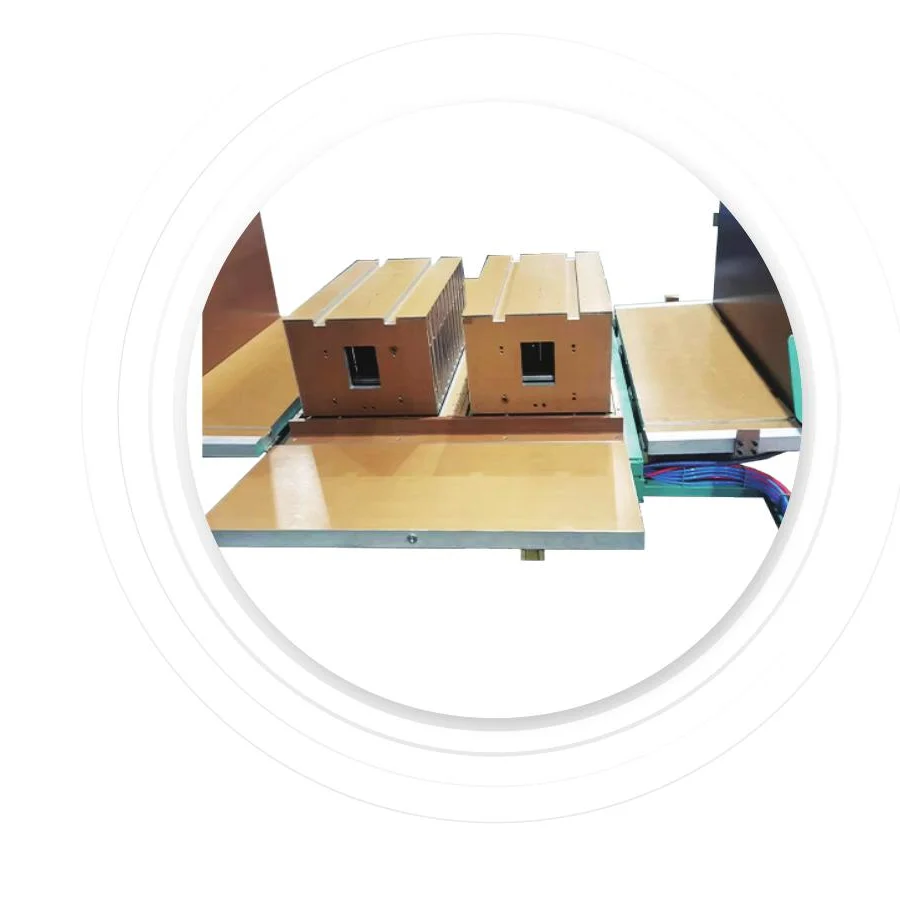
Refrigerator-Grade Moulds
Vacuum-forming + foaming moulds engineered to your cabinet/door geometry. Custom mould design service available.
Learn moreService & Support
Warranty & Service
On-site intervention available in every region where we have delivered projects.
On-Site Installation
Our engineers fly to your factory to supervise installation, layout verification, and first-run production.
Commissioning + Tuning
Trial run + parameter tuning to your local raw material, climate, and target product spec — until throughput meets contract.
Operator Training
5-10 day on-site training for production team, QC, and maintenance — bilingual manuals + video tutorials provided.
3-Year Warranty + Spares
Core equipment 3-year warranty, electrical 2-year. Spare parts in stock with global express shipment 24h dispatch.
Pertanyaan Umum
Three layout forms — ground rail, linear, rotary door — how do I pick?
How much factory space and ceiling height do I need?
What heating method should I pick — steam or oil?
What blowing agent / foaming material does each line support?
How many people does it take to run each line?
What about integration with my existing assembly, refrigeration loop, and packaging lines?
How long does installation + commissioning take?
What's the warranty, spare parts, and service coverage?
Can I upgrade from ground rail to add a rotary door line later?
What about cyclopentane safety — is the line ATEX-rated?
Butuh solusi pendingin lengkap?
UREXCEED mengintegrasikan cetakan, mesin foam, lini produksi & material dari 6 pabrik mitra. Beri tahu target kapasitas Anda, 24 jam kami sampaikan konfigurasi & penawaran.