Supermarket Refrigerated Cabinet Foaming Specialty Machine — lignes de production by UREXCEED. Lead time 60 – 90 days, MOQ 1 set.

Supermarket Refrigerated Cabinet Foaming Specialty Machine
Linear hydraulic specialty foaming machine for supermarket service cabinets, convenience store back-warehouse refrigerators and restaurant chain prep refrigerators. Water-heated + air-cooling, 380 kW peak, 200–600 cabinets/shift.
Start with an engineering scope review
Send dimensions, target output and drawings. Response timing follows project complexity and working hours.
Spécifications
- Layout Form
- Supermarket service-cabinet foaming specialty (linear, hydraulic)
- Drive Method
- Hydraulic
- Heating Method
- Water heating + air-cooling (PID-controlled)
- Number of Stations
- 1 (single-cabinet specialty)
- Cabinet Size Range (L×W×H)
- 2,000 × 2,000 × 735 mm (typical supermarket service unit)
- Footprint (Overall L×W×H)
- Approx. 80 × 400 × 525 mm
- Foaming Material
- POL + Cyclopentane + ISO / POL + HCFC-141a + ISO / POL + HCFC-245fa + ISO
- Voltage / Frequency
- 380V · 50 Hz · Control voltage 24V
- Total Power
- Approx. 380 kW (peak)
- Compressed Air Requirement
- 0.5 MPa
- Best Fit Capacity
- ~200 – 600 cabinets per shift
- Lead Time
- 60 – 90 days
- MOQ
- 1 set
Applications
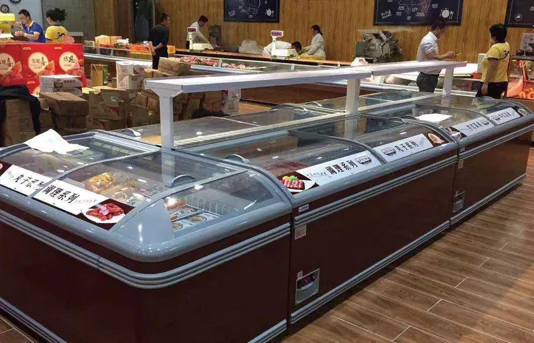
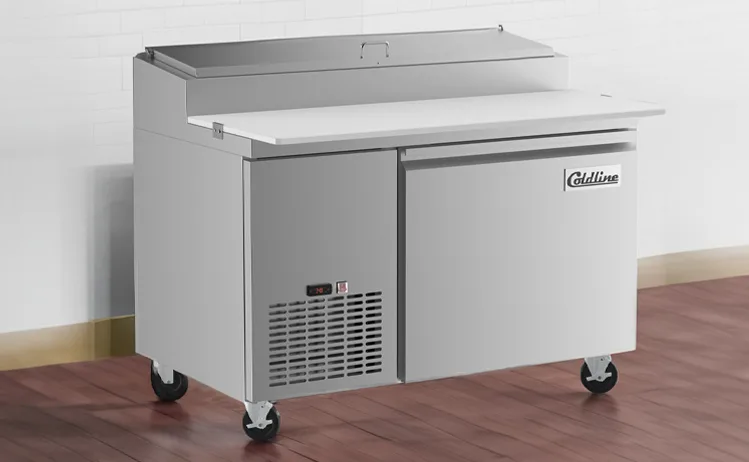
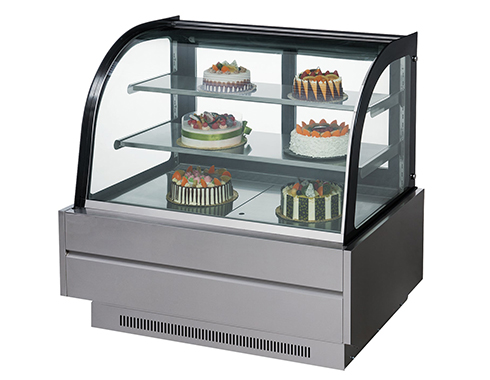
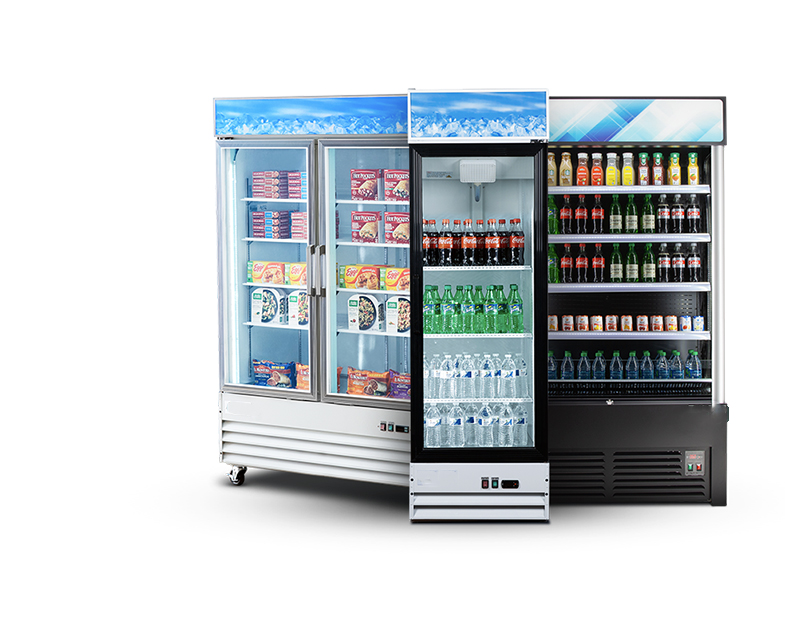
- Supermarket fresh-food service cabinet (storage cabinet for chilled produce)
- Convenience store back-warehouse refrigerated cabinet
- Restaurant chain prep refrigerator
- Retail chain refrigerated storage cabinet
- Cold-chain warehouse intermediate storage cabinet
Integrated foaming equipment
Machine de pulvérisation PU
Système d'isolation mobile, 5–20 kg/min
When a refrigerator factory actually needs a spray foam machine
Most refrigerators get foamed in closed moulds with a high-pressure machine. Spray foam is for the cabinets where the closed-mould approach hits a wall. Four clear cases:
Oversized cabinets
Cabinet too big for a practical mould. Supermarket island freezers, 2–4 m long open-top display cases, walk-in commercial cabinets. A 4m steel mould costs USD 150K+ and weighs tons. Spray foam handles the same job at a fraction of the capex.
Irregular geometry
Irregular or curved geometry. Curved-front commercial freezers, dome-shaped display refrigerators, faceted product-specific cabinets where a closed mould would need 6+ parting surfaces.
Thick walls
Thick walls (over 50mm). Pharmaceutical / vaccine ultra-low-temperature freezers (-86°C) need 60–80mm of insulation. A closed mould at that thickness has cure-time and stress problems. Spray-applied multi-layer foam handles thick walls cleanly.
On-site work
On-site work. Refrigerator inner liner defect repair (bubbles, sink marks discovered before export), retrofit insulation on existing cabinets, custom one-off cold rooms attached to refrigerator factories.
Our spray gun and heated hose system
The gun and the heated hose are the parts of the machine where most quality problems start. We use proven, commercially-available components for both.

Spray gun
Spray gun: industrial-grade, comparable in design to Graco Fusion / Wagner GX class. Air-purge head (no solvent flush needed), variable fan pattern 15°–60°, replaceable mix chamber. Replacement gun tips and mix chambers are stocked in our spare parts depots.
Heated hose
Heated hose: full-length electric heating with PID control, ±3°C across the entire hose length. Available in 10 / 20 / 40 / 60m configurations. Properly heated hose = consistent foam; a "cold spot" in the hose causes poor mixing and bad cell structure.
Electronic proportioner
Electronic proportioner with ±1.5% ratio accuracy. Polyol-to-ISO ratio is critical for spray foam — drift outside ±2% and you get under-cured surface foam (sticky, weak) or over-cured (brittle, dusty).
Tank feed
Drum-direct or day-tank feed. Drum-direct is simpler (drop pumps into 200L drums); day-tank is needed for high-volume continuous spraying or when you're drawing from bulk storage.
PLC control
PLC with recipe storage (typically 10–20 recipes). Stores temperature, pressure, ratio setpoints per polyol grade.
Five refrigerator scenarios we ship this machine for most
Here's where this machine actually goes in refrigerator factories — these account for ~80% of the units we ship.
Supermarket island freezers
Supermarket island freezers (open-top, 2–4 m long). Foam volume 30–80 kg per cabinet, sprayed in 30–60 minutes. Typical sprayer output 100 island cabinets per week, single operator.
Long commercial displays
Long commercial display cabinets (8–12 m single-piece, retail freezer aisles). Foam volume 80–150 kg per cabinet. These are often single-piece custom orders, where a mould investment makes no sense.
Ultra-low-temp pharma freezers
Pharmaceutical / vaccine ultra-low-temperature freezers (-86°C, thick-wall 50–80 mm). Foam volume 40–70 kg per cabinet, sprayed in 2–4 layers.
Inner liner repair
Inner liner defect repair on finished refrigerators. Quick spot-spray of bubbles, voids, sink marks before export. Recovers 2–5% of cabinets that would otherwise be scrapped — significant on a 500K-unit/year factory.
Large chest freezers
Large chest freezers (800L+) and walk-in commercial cabinets where a closed mould would weigh too much to be practical.
Spray vs press foam — the honest comparison
Spray is a different process. Different cell structure, different density, different k-factor. Worth being clear about what you gain and lose.
| Metric | Spray-applied | Press / mould foamed |
|---|---|---|
| k-factor (W/m·K) | 0.022 – 0.024 | 0.018 – 0.020 |
| Molded density (kg/m³) | 40 – 50 | 32 – 38 |
| Closed cell content | 88 – 92% | 95%+ |
| Cabinet wall thickness range | 20 – 100 mm flexible | typically 35 – 60 mm |
| Setup cost per cabinet design | Low (no mould) | High (USD 30K – 200K mould) |
| Output rate | Slower (sprayer-limited) | Faster (mould cycle) |
So: spray foam for cabinets where you can't practically build a mould or where you only need a few units of a design. Press foam for high-volume mainstream refrigerators. The slight loss in k-factor (about half an energy class) is the trade for the geometric flexibility.
Mobile, containerized, or stationary — three deployment patterns
How you deploy the machine inside (or outside) your factory matters as much as the machine spec itself.
Mobile cart configuration. Whole machine on industrial wheels, 1.5 × 1 m footprint. Roll it to where the cabinet is, plug into a nearby socket and air supply. Best for low-volume operations where the cabinet doesn't fit through a doorway to the foaming room. Most popular for repair work and one-off custom cabinets.
20' container-mounted configuration. The entire machine + air compressor + drum storage lives inside a shipping container. Drive the container to a temporary site (large display cabinet install at a supermarket, a custom cold room project), open the doors, run spray hoses out to the work zone. Used by refrigerator factories that do on-site installation work.
Stationary in-line configuration. Machine bolted to the factory floor, multiple spray hoses fed to dedicated spray booths. Best for refrigerator factories that have a dedicated spray foam product line (e.g. supermarket island freezers as a continuous product).
MDI exposure and operator safety — the biggest single risk
Of all the equipment in a refrigerator factory, the spray foam machine has the highest occupational health risk. Atomized MDI aerosol is genuinely hazardous to lungs. Done right it's manageable; done wrong it causes long-term respiratory damage. We don't sell this machine without the safety pack.
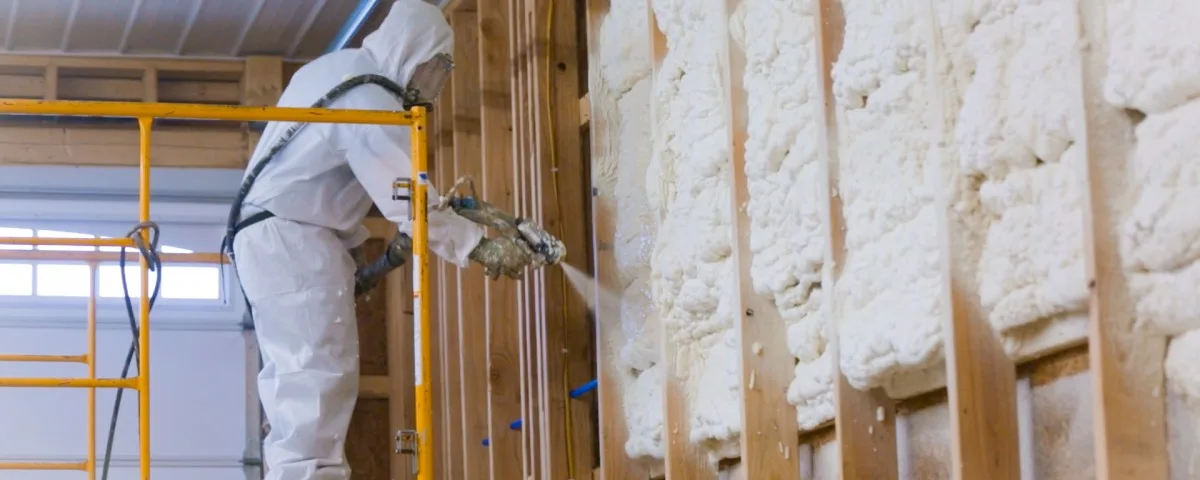
Supplied-air respirator
Supplied-air respirator (positive-pressure full-face hood with hose-fed clean air from outside the spray zone). NIOSH-approved. This is the only respirator that reliably keeps MDI exposure below ACGIH TLV (5 ppb). Filter cartridges are not sufficient for sustained spraying.
PPE (Tyvek, gloves, boots)
Tyvek coverall, butyl gloves, boot covers. Disposable, replaced every shift. MDI penetrates ordinary cotton/nylon fabric.
MDI vapor monitor
Real-time MDI vapor monitor at the spray zone perimeter. Calibrated to ACGIH TLV. Triggers alarm if vapor leaks outside the spray booth (usually means ventilation failure).
Spray booth ventilation
Spray booth ventilation design spec we provide: minimum 6 air changes per hour, exhaust at floor level (MDI aerosol settles), inlet air at ceiling level. Booth pressure slightly negative to surroundings.
Medical surveillance
Recommended (and required in many EU countries) annual medical surveillance for sprayers — lung function testing, respiratory symptom questionnaire. We can connect you with occupational health providers.
Operator training
Operator training covers: putting on PPE in correct order, breathing apparatus checks, what to do if a hose fails or the monitor alarms, decontamination procedure at end of shift. Initial training 3–5 days, refresher every 6 months.
Compatible PU formulation — spray-grade is different
You can't use your high-pressure cyclopentane polyol on a spray machine. Spray foam needs a chemistry that gels in 3–5 seconds (not 40–60), has higher viscosity (so it sticks to vertical walls instead of running down), and uses a different surfactant balance. We supply the matching system.
Fast gel time
Cream 2–4s, gel 3–6s, tack-free 8–15s. About 8–10× faster than press-foam recipes. This is what lets you build up 50mm of foam in 2–3 passes without it sagging.
Higher viscosity
Polyol viscosity 6,000–12,000 mPa·s (vs 3,000–6,000 for press foam). Higher viscosity = better vertical-wall hang.
Higher density
Free-rise density 35–45 kg/m³ (vs 22–28 for press foam). Higher density compensates for the lower cell-structure quality.
HFO over cyclopentane
HFC-245fa or HFO-1233zd(E) are the standard blowing agents for spray. Cyclopentane is technically possible but the open-air spraying creates an explosion risk that's much harder to mitigate than in a closed-mould setup. Most spray operations use HFO.
Operator training — this isn't a "press the button" machine
Spray foam is a craft skill. A good sprayer's output is double a beginner's, and quality is much more consistent. We send a trainer to your factory for 2 weeks of supervised training before unattended production.
Spray distance
Spray distance: 30 cm ±5 from substrate. Too close → uneven thickness, splash-back. Too far → cold spots, poor adhesion.
Fan angle
Fan angle: matched to substrate. Wide fan (50–60°) for flat walls. Narrow fan (15–25°) for corners and edges.
Pass overlap
Pass overlap: 50% with the previous pass. Less than 50% → striping pattern in finished foam. More → uneven thickness.
Multi-layer build
Multi-layer build: wait for previous layer to gel (touch test) before next pass. Typical wait 30–60s. Skipping this wait causes heat buildup, foam structure damage.
Pattern direction
Pattern direction: alternate orientation each layer (horizontal pass 1, vertical pass 2, horizontal pass 3). Helps even out thickness variance.
Production ramp
Production ramp: new sprayer reaches steady quality at about day 7. Full production speed about day 14. We stay through both stages.
The supermarket service cabinet foaming specialty machine targets one specific buyer: supermarket / convenience store / restaurant chain back-warehouse refrigerated cabinet OEMs. These cabinets are different from household refrigerators — heavier-duty, longer 24/7 duty cycle, often custom-sized to store fixtures. The specialty machine ships with the heated-jacket profile and PU recipe density tuned for this end use.
Why supermarket cabinet OEMs need a specialty machine
Generic refrigerator lines run a standard PU recipe and fixture profile. Supermarket service cabinets need (a) higher foam density for 24/7 duty cycle endurance, (b) longer cure time at higher temperature for thicker walls, and (c) larger cabinet sizes (up to 2 m length common). This specialty machine ships with those tuning built-in — no retrofitting a generic line.
Four reasons to buy a supermarket-specific foaming specialty over a generic line
Data-driven advantages of the supermarket-targeted specialty configuration.
Higher PU foam density 38–45 kg/m³ for 24/7 duty cycle
Generic household refrigerator foam runs 32–36 kg/m³ for 12-hour daily use. Supermarket cabinets (24/7 always-on) need 38–45 kg/m³ density to resist long-term thermal cycling. The specialty machine ships with PU metering profile calibrated to higher density without modification.
Water heating + air-cooling for longer curing profile
The dual heating + cooling system supports the longer 8–15 minute cure cycle (vs 6–10 min household) needed for thicker cabinet walls (50–80 mm vs 30–45 mm household). Active cooling reduces post-mould warp risk.
Cabinet size range 2,000 × 2,000 × 735 mm — supermarket service standards
Cabinet envelope fits the standard 2 m supermarket service cabinet + back-warehouse storage cabinet. Generic small-cabinet lines (1,500 × 800 mm) require custom fixture for these sizes.
Capacity 200–600 cabinets/shift — fits mid-size supermarket OEM
Output range targets supermarket-cabinet OEM factories producing 1,000–5,000 cabinets/month. Below 200/shift: single-station works. Above 600/shift: investment doesn't scale — better build full 6/8 station linear line.
How the supermarket cabinet cycle runs
Single-station specialty cycle with longer cure + cool profile (~3 minutes per cabinet, manual handling between cycles).
- 1
Pre-prep — operator loads pre-skinned 2 m supermarket cabinet shell + custom shelving brackets onto fixture. Position-check with laser reference. ~45 sec.
- 2
Mould close + cyclopentane inject — hydraulic clamp engages. PU machine meters 2.5–4.5 kg POL+ISO+cyclopentane per cabinet (depends on wall thickness). ~25 sec.
- 3
Heated cure — water-jacket heats fixture to 50–58°C. Foam rises and cures over 8–12 min. PLC monitors per-station thermocouple temperatures.
- 4
Active cool — air-cooling kicks in after cure complete, drops cabinet from 50°C to 25°C before demould. Reduces warp from rapid handling. ~2 min.
- 5
Demould + QC — operator opens mould, lifts cabinet onto inspection conveyor. Visual + spot-density check before downstream gasket / refrigeration assembly. ~30 sec.
FAQs — supermarket refrigerated cabinet foaming specialty machine
How is this different from a household refrigerator foaming machine?
Investment + lead time?
Capacity for 1,000 cabinets/month — is this the right machine?
Can we scale up to 5,000 cabinets/month?
What end-product applications fit?
Does it support glass-door variants?
Produits associés
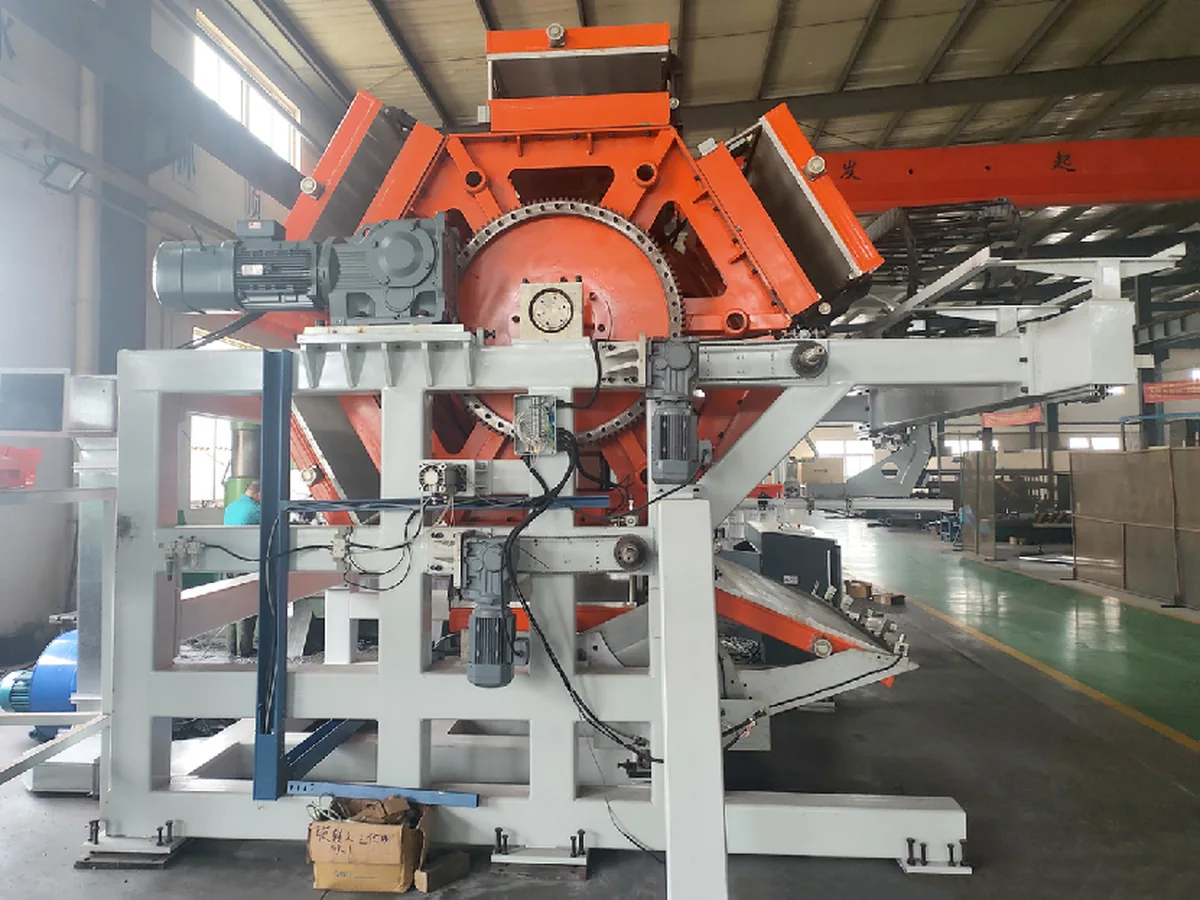
4-Station Hydraulic Air-Curtain Cabinet Foaming Fixture
4-station hydraulic foaming fixture for air-curtain refrigerated display cabinets (open-front merchandisers up to 4 × 1.8 × 0.55 m). Top/bottom flat-pressing clamp, water heating, 50 kW, 80–200 cabinets/shift.
Ligne de panneaux frigorifiques
Ligne continue, 10–40 panneaux/h, 50–200 mm
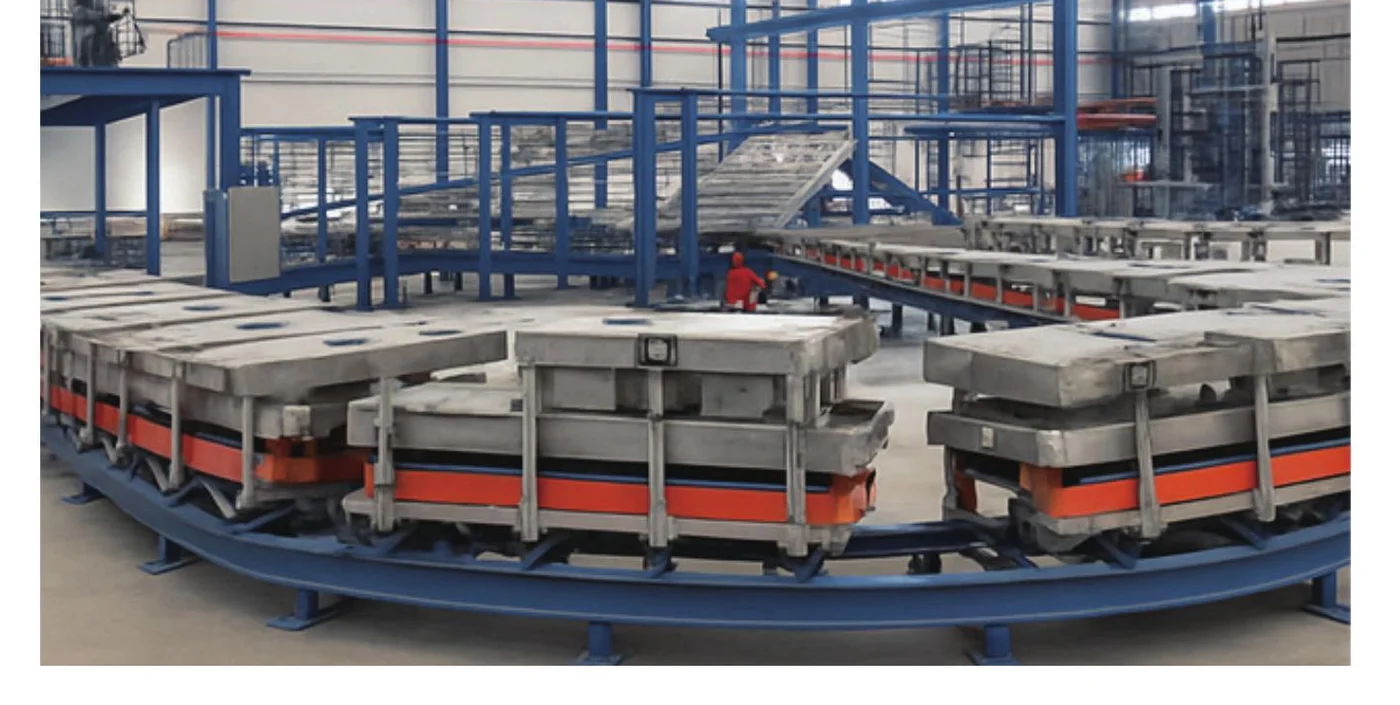
26-Station Refrigerator Door PU Foaming Line
Closed-loop ground-rail PU foaming line dedicated to refrigerator and cabinet DOOR foaming. 26 single-cavity fixture stations on a continuous steel track, 20-sec takt, ~1,200 doors per 8-hour shift (~2,450/day on two shifts) at 85% line efficiency. 2,000 × 900 mm fixture × 200 mm closing height — sized for door panels. Cyclopentane + ATEX Zone 1, steam or oil heating.
Cross-Sell · One-Partner Synergy
Match Your Production Line With Factory Solutions
Pick the factory type that matches your buyer market — we engineer the complete production line for that vertical.
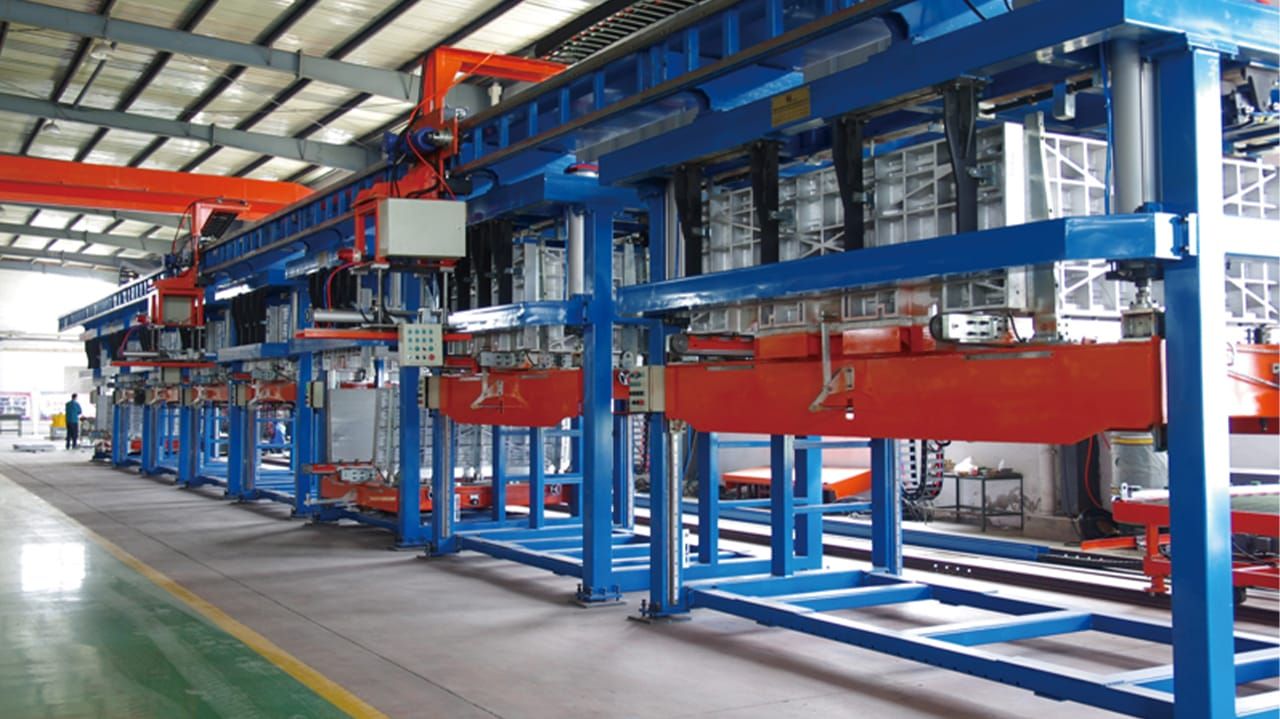
Browse 13 Factory Solutions
Refrigerator / Chef Base / Freezer / Display Cabinet / Commercial Freezer + 8 specialized markets.
Learn more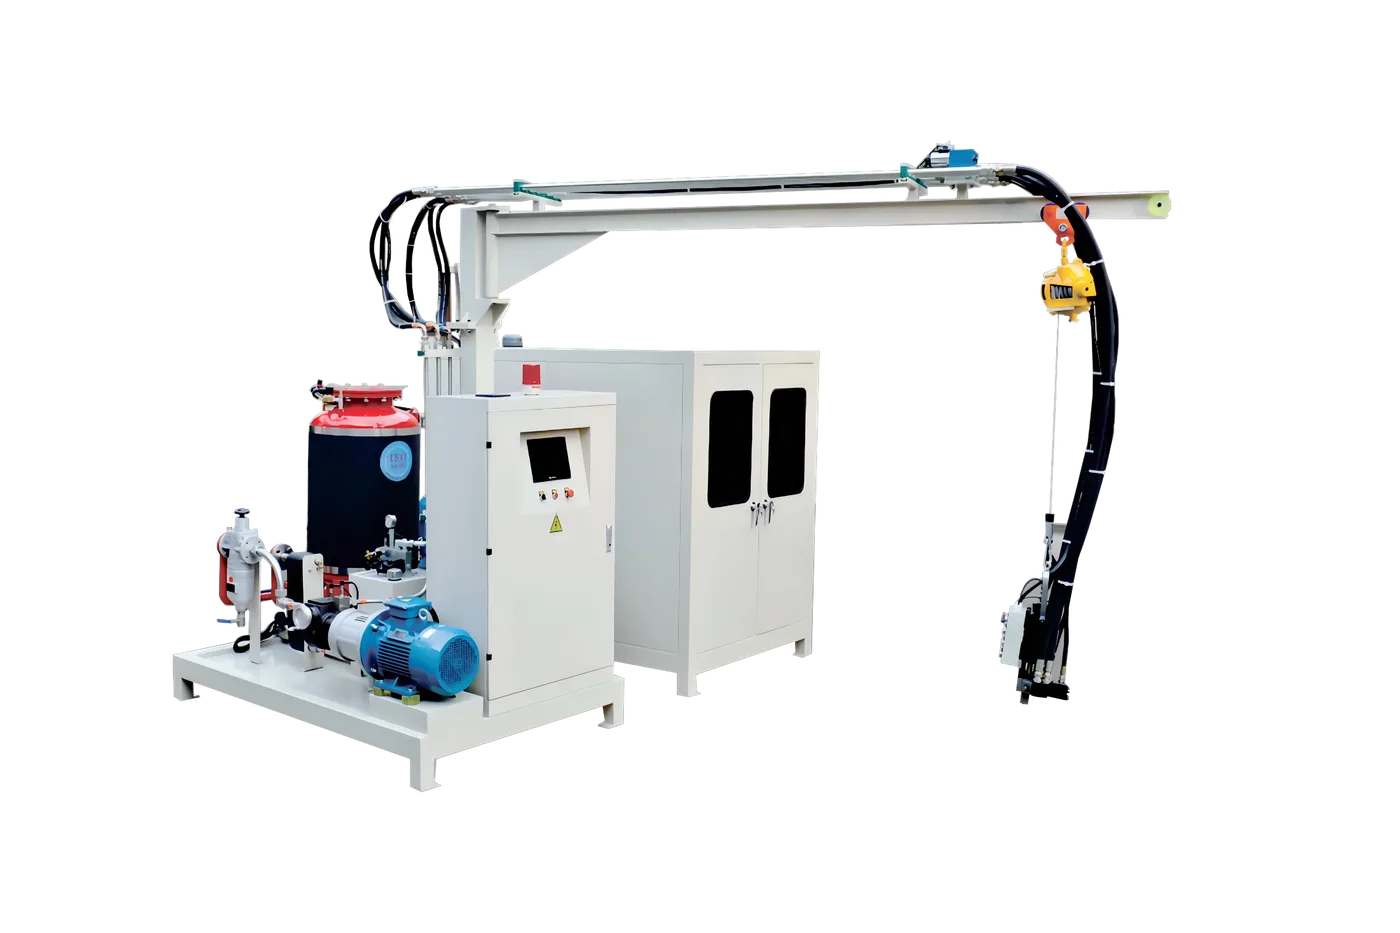
PU Foaming Machines
High-pressure (cyclopentane / 2C / 3C) + low-pressure + spray-foam — pick the foaming line that matches your factory.
Learn more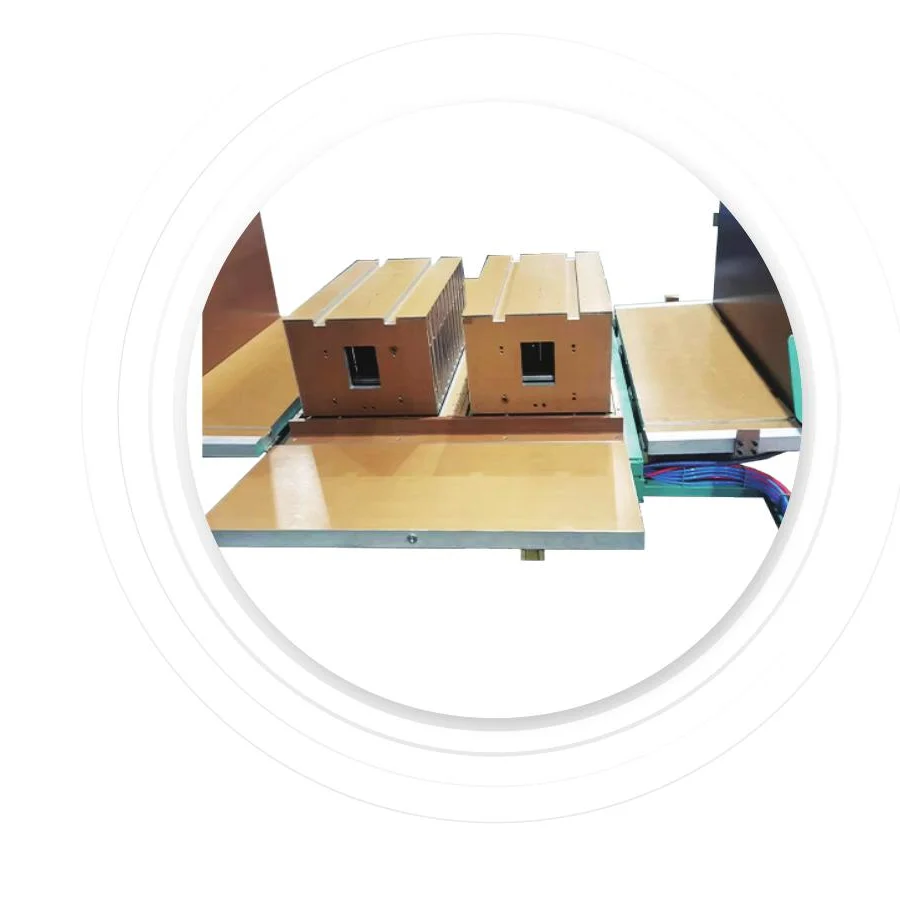
Refrigerator-Grade Moulds
Vacuum-forming + foaming moulds engineered to your cabinet/door geometry. Custom mould design service available.
Learn moreService & Support
Garantie & Service
Intervention sur site disponible dans chaque région où nous avons livré des projets.
On-Site Installation
Our engineers fly to your factory to supervise installation, layout verification, and first-run production.
Commissioning + Tuning
Trial run + parameter tuning to your local raw material, climate, and target product spec — until throughput meets contract.
Operator Training
5-10 day on-site training for production team, QC, and maintenance — bilingual manuals + video tutorials provided.
3-Year Warranty + Spares
Core equipment 3-year warranty, electrical 2-year. Spare parts in stock with global express shipment 24h dispatch.
Questions fréquentes
Quel est le délai de livraison typique ?
Quelle est la quantité minimale de commande ?
Proposez-vous la personnalisation et l'OEM / ODM ?
Quelles certifications ce produit possède-t-il ?
Besoin d'une solution complète de réfrigération ?
UREXCEED intègre moules, machines de moussage, lignes de production et matériaux au sein de 6 usines partenaires. Indiquez-nous votre objectif de capacité et nous répondrons avec une configuration et un devis sous 24 heures.