Single-Station Linear Cabinet Foaming Specialty Machine — производственные линии — холодильники, морозильники, холодильные камеры под ключ by UREXCEED. Lead time 60 – 90 days, MOQ 1 set.
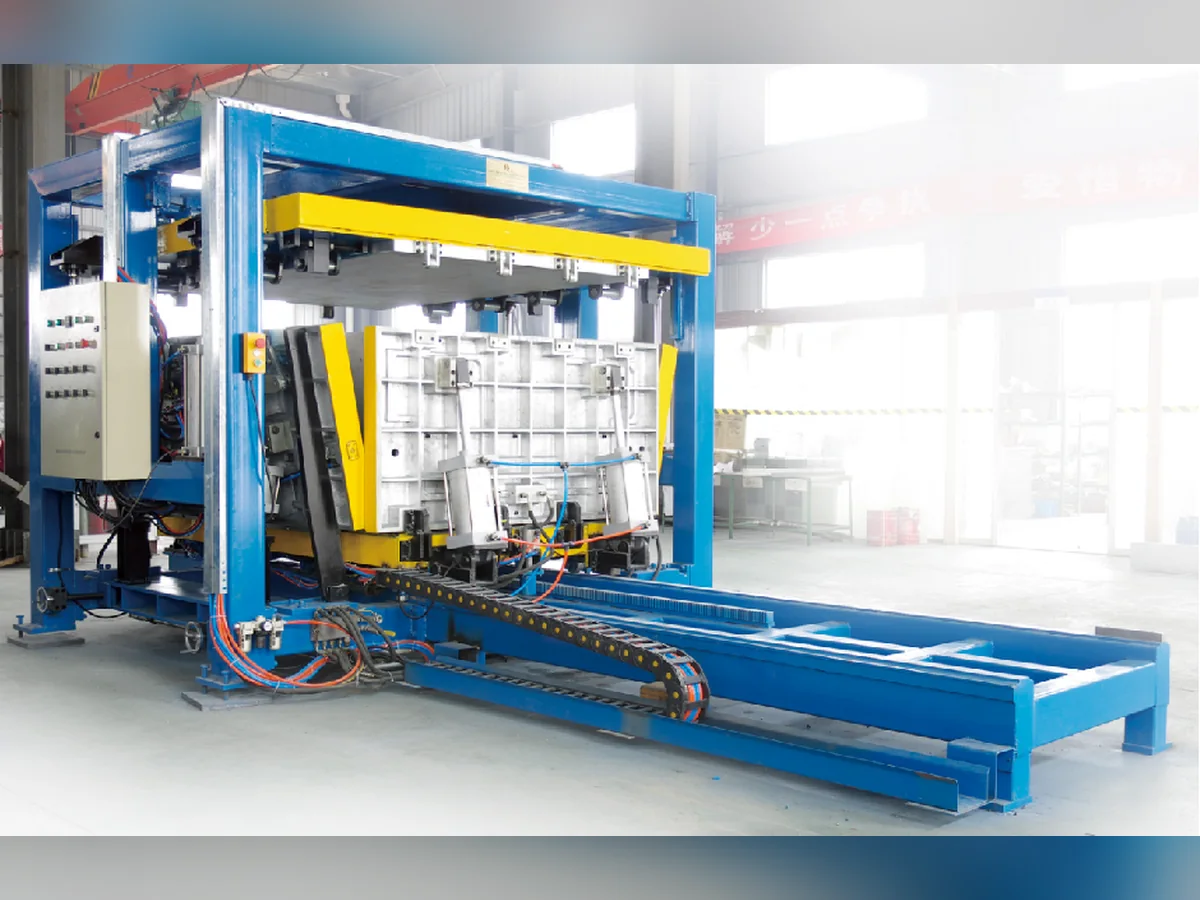
Single-Station Linear Cabinet Foaming Specialty Machine
Single-station hydraulic linear specialty foaming machine for refrigerator cabinet R&D, sample runs and low-volume production. Same fixture template as 11-station main line — use for mould trial and PE/EPP wave-type chest freezer samples before full-line production.
Start with an engineering scope review
Send dimensions, target output and drawings. Response timing follows project complexity and working hours.
Характеристики
- Layout Form
- Single-station linear cabinet foaming specialty machine
- Drive Method
- Hydraulic clamping
- Heating Method
- Water heating (PID-controlled)
- Number of Stations
- 1 (single-station specialty)
- Cabinet Size Range (L×W×H)
- 2,000 × 2,000 × 735 mm
- Footprint (Overall L×W×H)
- Approx. 80 × 400 × 525 mm
- Foaming Material
- POL + Cyclopentane + ISO / POL + HCFC-141a + ISO / POL + HCFC-245fa + ISO
- Voltage / Frequency
- 380V · 50 Hz · Control voltage 24V
- Total Power
- Approx. 380 kW (peak)
- Compressed Air Requirement
- 0.5 MPa
- Best Fit Capacity
- ~150 – 400 cabinets per shift (R&D / pilot / sample run)
- Lead Time
- 60 – 90 days
- MOQ
- 1 set
Применение
- R&D / sample / mould trial runs for new cabinet variants
- Low-volume specialty cabinet production (<500 cabinets/day)
- PE / EPP foaming station for in-mould trial of insulation board
- 1986 type / 1700 type / 1186 type chest freezer trial production
- PE / EPP wave-type chest freezer cabinet sample foaming
- Custom cabinet design verification before tooling main production line
Integrated foaming equipment
Пенообразующая машина низкого давления
5–100 г/с, динамическое смешение, баки 40–250 л
When a low-pressure machine actually beats a high-pressure one
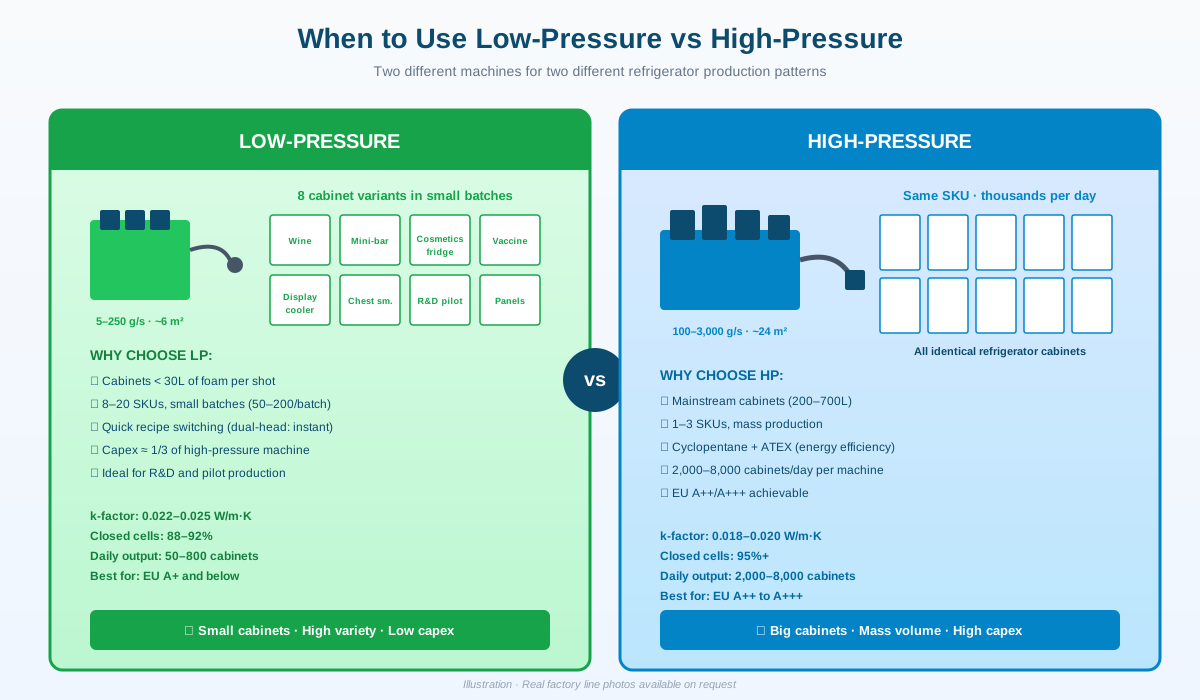
Most refrigerator factories should buy the high-pressure machine. But there are three situations where the low-pressure version is genuinely the right call.
Small cabinets
Small cabinets (under ~30L of foam per shot). The high-pressure machine's minimum reliable shot is ~50g; below that the mixing head doesn't reach steady state. Wine cabinets, mini-bars, vaccine boxes typically need 5–25g shots. Low-pressure handles them naturally.
Many small-batch variants
Many small-batch variants. If you build 8–20 cabinet SKUs in batches of 50–200 each (typical for wine cabinet OEMs, hotel mini-bar suppliers, medical cold storage), recipe-switching time dominates. The dual-head low-pressure config swaps recipes instantly. The HP machine purges for 10+ minutes between recipes — that's 30% of your shift on recipe changes alone.
R&D and pilot runs
R&D, pilot runs, sample production. New cabinet designs need 1–2 weeks of trial foaming to dial in. The HP machine's big day tanks mean every recipe iteration wastes 10–20kg of material. The LP machine's 40–80L tanks make each iteration cost a fraction of that.
Capex constraints
Capex is 1/3 of the HP machine. If you're a startup or testing market demand for small refrigerators, the LP machine lets you start production with a fraction of the upfront cost.
What's inside the low-pressure machine
Mechanically simpler than the HP machine, which is the point. Fewer moving parts, easier to maintain, easier to train operators on.
Dynamic mixer
Dynamic mechanical mixing — a motor-driven impeller in the mixing head. The polyol and ISO enter the mixing chamber separately and the impeller mixes them at 2,000–3,000 RPM. Less homogeneous than HP impingement, but adequate for cabinets where k-factor isn't the headline spec.
Smaller tanks
Smaller jacketed day tanks (40 / 80 / 160 / 250L per component). Electric jacket heating, PID ±1°C. No N₂ blanket needed (the lower throughput and smaller tanks mean atmospheric moisture isn't a problem).
Dispensing gun
Hand-held or fixed-position dispensing gun. Cycle time per shot is 8–60 seconds (programmable). Most factories run hand-held for flexibility.
Simpler PLC
Simpler PLC (Siemens S7-200 SMART or Mitsubishi FX5) — recipe storage, output adjustment, basic temperature logging. No remote diagnostics on the base spec (available as upgrade).
Optional dual head
Optional dual-head configuration. Two mixing heads on the same machine, one for each recipe. Instant recipe swap without purging — for factories running many cabinet variants.
Eight small-refrigerator scenarios we ship this machine for
The low-pressure machine isn't a "general purpose" machine — it's specifically for these refrigerator categories where HP overkill and HP recipe changeover cost dominates.
Wine cabinets (28 / 46 / 100 / 180 bottle). Multiple SKUs per OEM, small batches, foam volume 3–8 kg per cabinet.
Hotel / dorm mini-bar refrigerators (20–50L). High variety (different countries, different OEM branding), small batches.
Cosmetics / skincare refrigerators (10–25L). Boutique product, dozens of designs, very small batches.
Breast milk / vaccine cold storage boxes. Often regulated, often custom-spec for the buying agency. Small volumes, high variant count.
Small beverage display coolers (table-top, 20–60L). Used in cafes, convenience stores, hotel rooms.
Built-in cabinet panel & shelf foaming for cabinets where the main shell is foamed elsewhere but smaller parts need separate foaming.
R&D pilot runs and sample cabinet production. Cheap to iterate, cheap to scrap a bad design and start over.
Small chest freezers (≤150L) — domestic / small commercial. Often regional brand variants.
Foam quality: low-pressure honest comparison
Worth being honest about the trade-off. Low-pressure foam is not as good as high-pressure foam. For cabinets where energy class is decisive, this matters. For most small refrigerators, it doesn't.
| Metric | Low-pressure | High-pressure |
|---|---|---|
| k-factor (W/m·K) | 0.022 – 0.025 | 0.018 – 0.020 |
| Closed cell content | 88 – 92% | 95%+ |
| Density consistency | ±8% | ±3% |
| Cell size uniformity | 150 – 250 µm | 100 – 180 µm |
| Practical EU energy class (2021 A–G label) | E to G, legacy A+ to A (cabinet dependent) | B to E, legacy A++ to A+++ |
Translation: for wine cabinets, mini-bars, vaccine boxes — where the buyer cares about size, looks, price, and reliability more than about energy class — the LP foam quality is fine. For mainstream household refrigerators going to EU consumers, run the HP machine.
Using this machine for R&D and pilot production
About a third of our LP machine customers buy it specifically as the R&D / pilot line. Here's how that typically works.
- 1
Week 1 — Concept and CAD: cabinet outer dimensions, inner volume, target market, target energy class, blowing agent choice (usually HFC or HFO at this scale, not cyclopentane).
- 2
Week 2 — Mould design and manufacture (we can do this in parallel — see our mould product family).
- 3
Week 3–4 — First trial foaming. Tune shot weight, cream time, gel time, mould temperature. Expect 5–10 iterations before the foam looks right.
- 4
Week 5 — Energy class testing (third-party lab). Measure k-factor and calculate cabinet energy consumption.
- 5
Week 6–8 — If energy class is short, re-formulate polyol blend. If cabinet geometry is the problem, modify the mould. Iterate.
- 6
Week 9–12 — Production sample run (50–200 cabinets) for buyer approval / certification.
- 7
Production-ready handover. Either keep using the LP machine for ongoing low-volume production, or step up to an HP machine if forecast volume justifies it.
What pairs with the low-pressure machine
Like with the HP machine, we engineer the chemistry around this specific equipment. Saves you the integration headache.
LP-grade polyol. We supply LP-grade polyol systems (typically water-blown or HFC-blown — cyclopentane is overkill at this scale). Smaller drum sizes (200L drums or 1,000L IBCs) match LP machine consumption rates.
Small refrigerator moulds. Small refrigerator moulds — typically aluminum, single cavity, simpler than the big steel cabinet moulds. We make these in parallel for first-time customers.
Browse our refrigerator-grade PU raw material system →The single-station linear specialty cabinet foaming machine is the R&D / pilot / sample-run sibling of the 11-station main line. Same fixture template, same PU recipe, same heating subsystem — but one station instead of eleven. Use it to verify a new cabinet design, run small-batch specialty SKUs, or trial PE/EPP wave-type chest freezers before committing to full-line tooling.
When the single-station specialty machine is the right buy
This machine is NOT a production line — it is a station. Pick it when (a) you need a sample-run setup before building a full 11-station main line, (b) your specialty cabinet volume is < 500 cabinets/day and a multi-station investment is overkill, or (c) you already have a main line but need a parallel station for irregular / non-standard variants. Many refrigerator OEMs run a single-station alongside their main line for R&D + small-batch.
Why a single-station specialty beats a full line for sample runs
Four reasons the single-station machine is the smarter buy for R&D / pilot / specialty work.
Same fixture template as 11-station main line — direct trial-to-production path
The 2,000 × 2,000 × 735 mm fixture matches the 11-station hydraulic mainline exactly. A design that runs clean on the single-station goes straight to mainline tooling — no re-engineering, no shape allowance. R&D cycle shortens by 4–8 weeks vs trialing on incompatible smaller machines.
Capex 60–75% lower than full 11-station line
Single-station investment ~ USD 180K–280K vs USD 750K–1.2M for a full 11-station hydraulic mainline. Fits within R&D budget envelopes without board approval for large capex.
150–400 cabinets/shift sweet spot — small-batch + variant trial covered
Single-station throughput handles small-batch premium SKUs (custom cabinet for hotel chain, vaccine refrigerator pilot) and runs unlimited variant trials per shift. Capacity scales linearly: 1 shift = 150–400 cabinets, 3 shifts = 450–1,200.
PE / EPP wave-type chest freezer specialty support
Multi-material flexibility — single-station supports PE / EPP wave-type chest freezer cabinet trials that need different PU recipe + fixture pressure profile vs standard ABS / PMMA cabinets. Switch between profiles in under 30 minutes between batches.
How the single-station cycle runs — 2-minute single-cabinet cycle
Each cabinet completes a full inject-cure-demould cycle in ~120 seconds. The operator works in parallel: while one cabinet cures, the next is being prepped.
- 1
Pre-prep (parallel) — operator loads pre-skinned cabinet shell + inner liner onto the fixture. Manual position-check with reference marks. ~30 sec.
- 2
Mould close + clamp — hydraulic clamp engages, locks fixture at ±0.05 mm parallelism. ~10 sec.
- 3
PU injection — POL + ISO + cyclopentane meter-mixed at 1.4–1.8 kg per cabinet, injected via single-head horizontal pour from one end. ~15 sec.
- 4
Cure — cabinet sits in heated fixture (45–55°C water-circulated jacket) while PU rises and cures. ~60–80 sec.
- 5
Demould — operator releases clamp, lifts cured cabinet free. Inspect for foam-density consistency before moving to downstream. ~15 sec.
FAQs — single-station linear cabinet foaming specialty machine
What is the lead time + investment?
Can it scale up to a full production line later?
How many cabinets per shift can it produce?
Operators per shift?
What materials and cabinet shapes does it handle?
When NOT to buy a single-station?
Сопутствующие товары
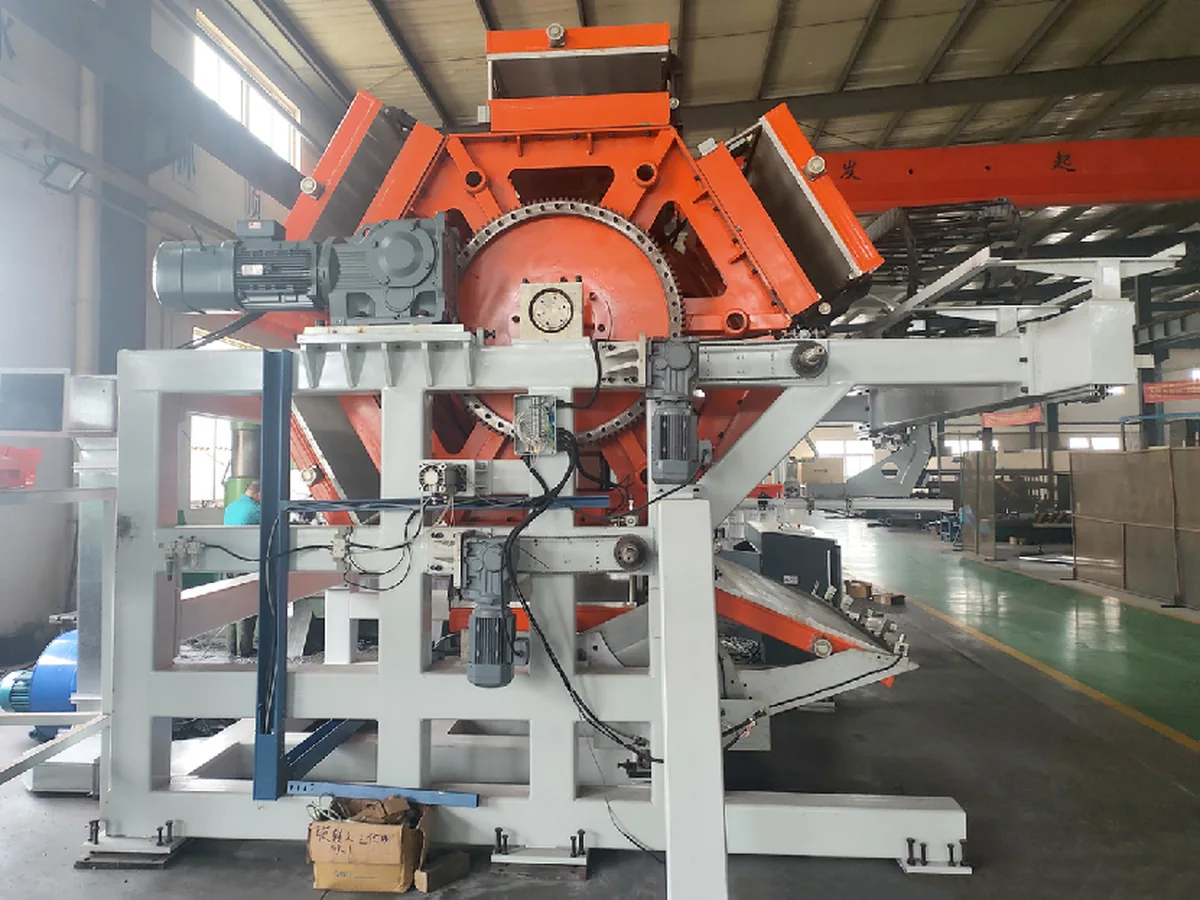
4-Station Hydraulic Air-Curtain Cabinet Foaming Fixture
4-station hydraulic foaming fixture for air-curtain refrigerated display cabinets (open-front merchandisers up to 4 × 1.8 × 0.55 m). Top/bottom flat-pressing clamp, water heating, 50 kW, 80–200 cabinets/shift.
Линия производства сэндвич-панелей
Непрерывная линия, 10–40 панелей/час, толщина 50–200 мм
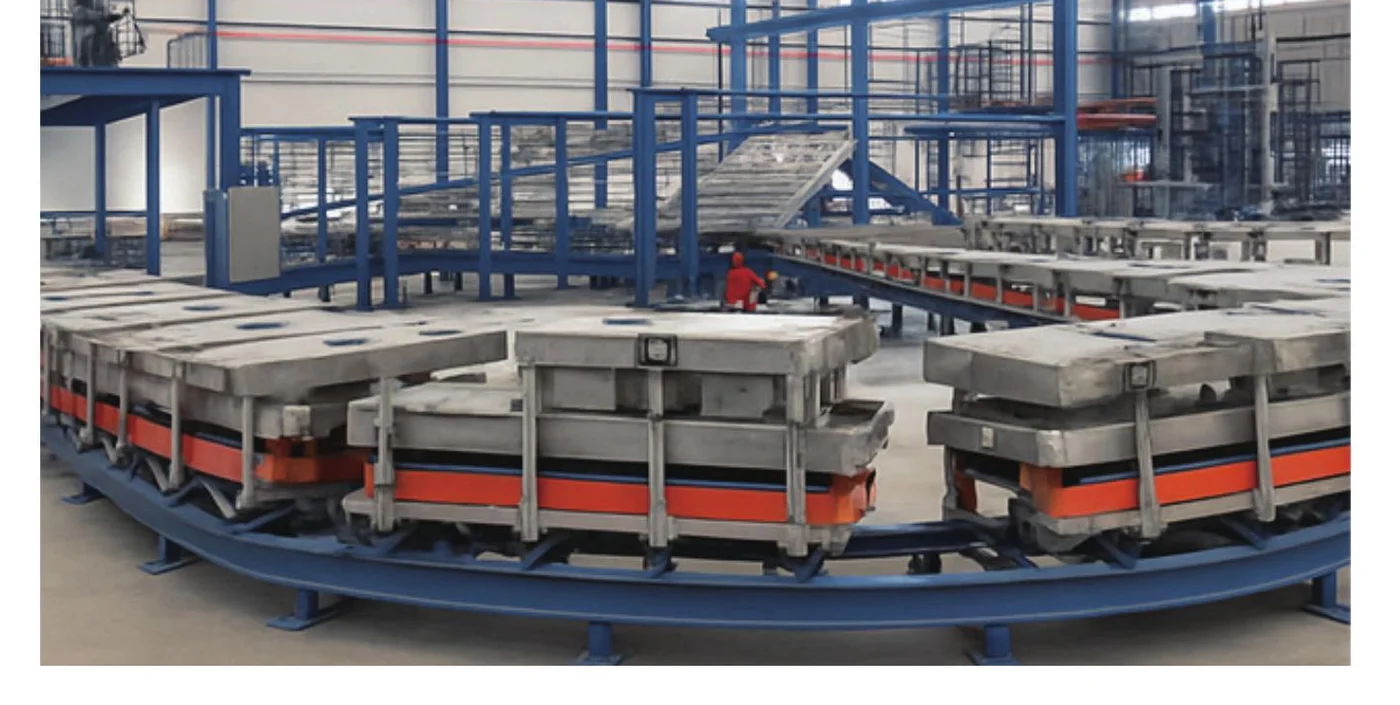
— 26-станционная напольно-рельсовая линия сборки холодильников (до 6 000 шкафов/смена)
the ground-rail line линия сборки холодильников: замкнутая напольно-рельсовая ППУ-вспенивающая линия для крупносерийных OEM производителей холодильников. 26 станций · 20-секундный цикл · ~3 000–6 000 шкафов/смена · паровой или масляный нагрев · ПОЛ + Циклопентан + ИЗО вспенивание.
Cross-Sell · One-Partner Synergy
Match Your Production Line With Factory Solutions
Pick the factory type that matches your buyer market — we engineer the complete production line for that vertical.
Browse 13 Factory Solutions
Refrigerator / Chef Base / Freezer / Display Cabinet / Commercial Freezer + 8 specialized markets.
Learn more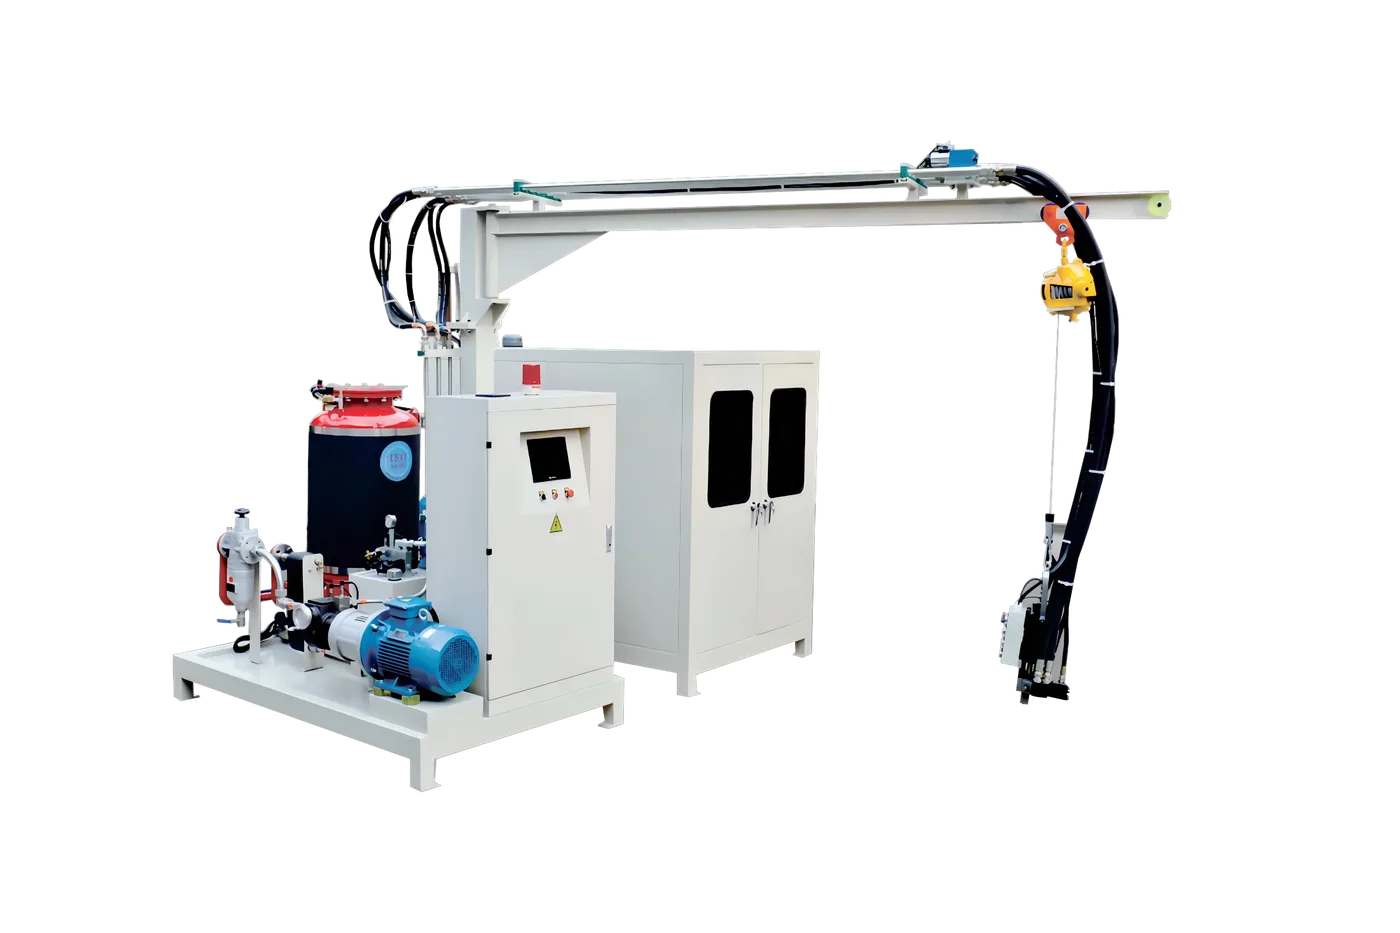
PU Foaming Machines
High-pressure (cyclopentane / 2C / 3C) + low-pressure + spray-foam — pick the foaming line that matches your factory.
Learn more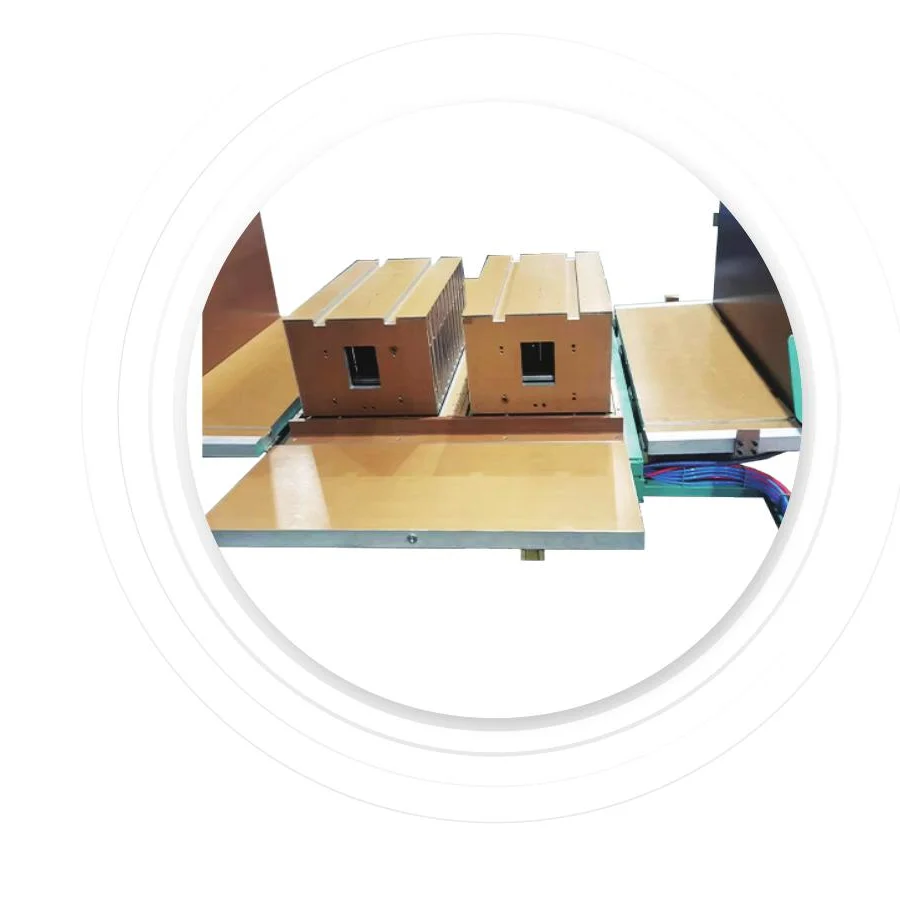
Refrigerator-Grade Moulds
Vacuum-forming + foaming moulds engineered to your cabinet/door geometry. Custom mould design service available.
Learn moreService & Support
Гарантия и сервис
Выезд на объект возможен во всех регионах, куда мы поставляли проекты.
On-Site Installation
Our engineers fly to your factory to supervise installation, layout verification, and first-run production.
Commissioning + Tuning
Trial run + parameter tuning to your local raw material, climate, and target product spec — until throughput meets contract.
Operator Training
5-10 day on-site training for production team, QC, and maintenance — bilingual manuals + video tutorials provided.
3-Year Warranty + Spares
Core equipment 3-year warranty, electrical 2-year. Spare parts in stock with global express shipment 24h dispatch.
Часто задаваемые вопросы
Какой обычный срок изготовления?
Какое минимальное количество заказа?
Предоставляете ли вы индивидуализацию и OEM / ODM?
Какие сертификаты имеет данный продукт?
Нужно комплексное холодильное решение?
UREXCEED объединяет формы, вспенивающее оборудование, производственные линии и материалы на 6 партнёрских заводах. Сообщите целевую производительность, и мы ответим конфигурацией и коммерческим предложением в течение 24 часов.